By Resodyn Acoustic Mixers, Inc.
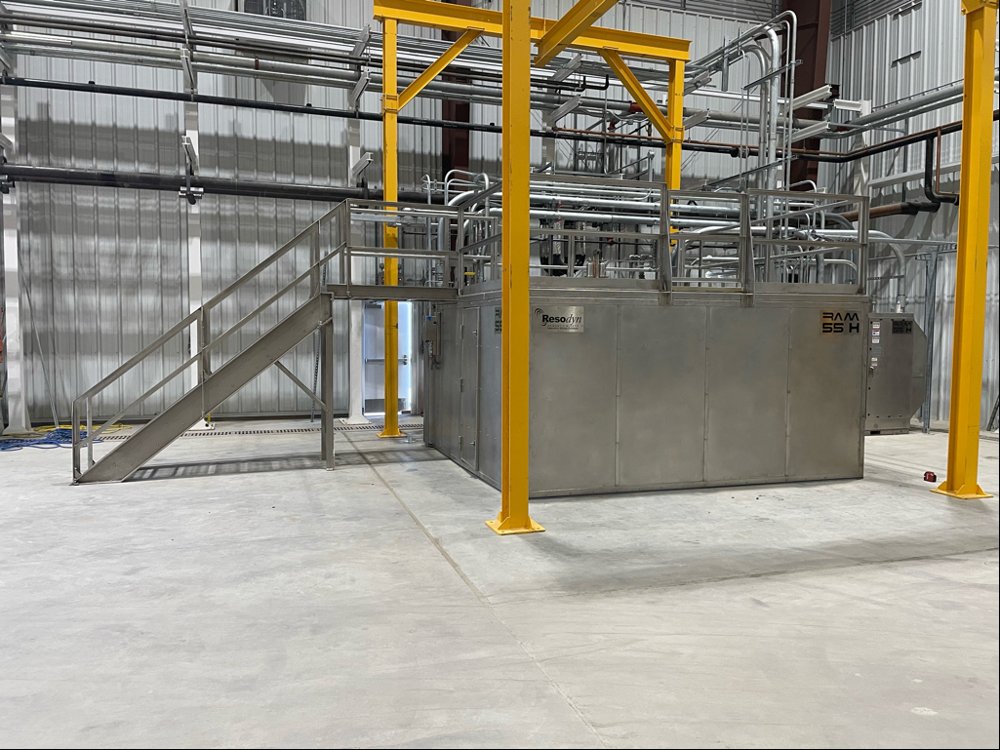
The Ultimate Scale for Pharmaceutical Production The RAM55 Pharma is the pinnacle of Resodyn's pharmaceutical production mixer lineup — delivering the full, transformative power of ResonantAcoustic® Mixing at a scale capable of supporting the largest commercial pharmaceutical manufacturing operations in the world. With a batch payload capacity of up to 924 lbs (420 kg), the RAM55 Pharma's digitally controlled, multiple processing capabilities multiply RAM's value through direct and easy scale-up from bench development to larger-scale batch production. The RAM55 Pharma enables the manufacture of a broad range of pharmaceutical products for less cost, more efficiently, more consistently, more uniformly, with less waste, and often with unprecedented results. Need a custom solution? All mixers can be customized for unique automations and applications. Enormous Mixing Capacity for Pharmaceutical Production The RAM55 does an enormous amount of work and produces results to match. RAM's bladeless system eliminates the extensive waste of material and time associated with traditional systems. Vessels are available in a variety of materials and up to 55 gallons (208 L) of capacity. It generally uses less power than other mixers of equivalent capacity. For large-scale pharmaceutical manufacturers — producing tablets, capsules, topical formulations, biologics, and other complex drug products — the RAM 55 Pharma eliminates the bottlenecks, quality variability, and compliance burdens that have long been associated with conventional impeller-based mixing at scale. Key Processing Capabilities - Processes up to 920 lb (417 kg) per batch - Handles solids, powders, liquids, gases, and viscous materials - Supports milling, grinding, sieving, and coating - Enables temperature control - Offers vacuum processing - Provides real-time monitoring and downloadable data for analysis - Stores up to 100 recipes for repeatable operations Key Advantages - 10–100x faster processing compared to traditional mixers - Highly repeatable results for consistent product quality - Direct scalability across the RAM product line - Exceptional ingredient distribution - Proven performance across global industries and applications Specifications General Model RAM55 Pharma Technology ResonantAcoustic® Mixing Intended Use Batch Mixing of Non-Hazardous Materials Unit Dimensions 10.5’ H x 15’ W x 10’ D (m: 3.2 x 4.57 x 3.05) Unit Weight Configuration-dependant Country of Origin USA Certifications Available CE, UL, CFR 21 Part 11 Operating Specifications Maximum Payload Capacity 920 lb (417 kg) Compatible Materials Solids, Liquids, Pastes, High Viscosity Max Vessel Acceleration 100g at approximately 60 Hz Temperature Control 200°F (93.3°C) to 23°F (-5°C) Vacuum Control 10 Torr Max Operating db > 80 db at 3’ Included Vessel Holder Assembly Application Specific Included Vessels Application Specific Control Specifications Human Machine Interface Full Color Touch Screen Operating System RAMWare™ Programable Mix Recipe Storage Yes Data Logging Yes Remote Operation Optional Control Features Up to 100 stored recipes, live monitoring, acceleration control Power Specifications Required Voltage 480 / VAC 60 Hz/3 Phase Documents - RAM55 product data sheet - McAlester Army Ammunition Plant's New Facility Accessories The RAM55 Pharma Production Mixer can be configured exactly how you need it. The Largest, Most Powerful Acoustic Mixer for Pharmaceutical Processing in the World Seamless Scale-Up from Bench to Batch One of the most significant advantages of the RAM 55 Pharma is how faithfully it preserves the formulation quality and process parameters established during early-stage R&D. RAM technology scales easily without additional testing from development to pilot to production scales — meaning the content uniformity, API distribution, and mixing profiles achieved on a PharmaRAM II or OmniRAM Pharma translate directly to the RAM 55 Pharma without costly revalidation or reformulation. This dramatically compresses the time between drug development and commercial launch. Contamination-Free, Sealed-Vessel Production The RAM 55 Pharma's bladeless, non-contact mixing architecture is particularly valuable at commercial production scale. Because mixing occurs in sealed containers using vibrational energy rather than impellers or blades, cross-contamination, operator exposure risks, and cleaning validation burdens are all minimized — all crucial for GMP compliance. For manufacturers producing multiple drug products on the same equipment, or working with highly potent APIs (HPAPIs), this is a decisive safety and regulatory advantage. Continuous Acoustic Mixing for Maximum Throughput Continuous Acoustic Mixing (CAM) systems are configurable for the RAM 55 Pharma and are custom built for the application, enabling high-throughput acoustic mixing of powders, pastes, and liquids without interruption. Resodyn's Continuous Acoustic Mixer creates ongoing production capacity of up to thousands of kilograms per hour — giving pharmaceutical manufacturers the throughput to meet global demand while maintaining the exacting uniformity and quality standards that patient safety requires. Trusted by the World's Leading Pharmaceutical Companies Resodyn Acoustic Mixers is the only company in the world to offer RAM technology, and provides pharmaceutical mixers geared toward the specific needs of pharmaceutical and medical industries. Resodyn has worked with demanding customers including well-known pharmaceutical manufacturers and top research institutions, all of whom rely on RAM's unique combination of speed, quality, and scalability to bring better medicines to market faster. The RAM 55 Pharma is not simply the largest pharmaceutical mixer Resodyn makes — it is the culmination of decades of acoustic mixing science, pharmaceutical industry expertise, and engineering excellence, all produced in Butte, Montana by one of the most innovative manufacturing companies in the American West. What is the RAM55 Pharma used for? The RAM 55 Pharma is a large-scale pharmaceutical acoustic mixing system designed for commercial production, pilot manufacturing, and advanced formulation processing in regulated pharmaceutical environments. What types of materials can the RAM55 Pharma process? The RAM 55 Pharma is designed to process a wide range of pharmaceutical materials, including powders, granules, slurries, suspensions, gels, creams, and high-viscosity pastes. What is the maximum batch capacity of the RAM55 Pharma? The standard capacity is rated at 920 lb (417 kg). But this is not the whole story. Capacity is affected by the material itself and its rheological properties, by the acceleration at which you are processing, and even the weight of your container. Your capacity could be significantly higher or lower than 920 lb (417 kg). Speak to your sales representative about your material and schedule a mix test for an accurate capacity based on your application details. How does acoustic mixing differ from traditional mixing methods? Acoustic mixing is the proven method of superior mixing and processing. It is bladeless, and is driven by vertical oscillation of the mix vessel at ~60 Hz and acceleration up to 100 g. Because the machine operates at resonance, it is energy efficient. The high energy motion drives mixing energy throughout the mix vessel for rapid and homogenous results beyond what conventional mixing can achieve. Traditional mixing methods vary, but generally rely on spinning paddles, tumbling vessels, or kneading action. Each method has significant limitations due to uneven energy distribution, excessive heat generation, slow processing, and material segregation. Simple mixing applications may achieve a suitable result, but the advanced processing needs commonly found in energetics, pharmaceuticals, advanced materials, batteries, additive manufacturing, and complex chemistries are often underserved by traditional mixing and processing methods. RAM is the processing technology that repeatedly solves the most difficult mixing, milling, coating, and chemical reaction challenges. What options are there for a RAM55 Pharma? The RAM 55 Pharma offers a variety of configurable options to support different pharmaceutical processing needs, including vacuum systems, jacketed vessels for temperature control, application-specific vessel designs, and automated process controls. Additional options include recipe storage, real-time process monitoring, data recording, material handling systems, and specialized vessel configurations for GMP and high-containment applications.
Laboratory Mixer The LabRAM II™ is a high-performance acoustic mixer designed to bridge the gap between laboratory development and mid-scale production. Engineered for speed, precision, and flexibility, it delivers efficient, highly repeatable mixing across a wide range of materials, from powders and liquids to viscous slurries. The machine can process 2.2 lb (1 kg). With an intuitive touchscreen interface, robust data tracking, and scalable processing capabilities, the LabRAM II™ enables faster formulation development while maintaining consistency from lab to production. Need a custom solution? All mixers can be customized for unique automations and applications. Built for Diverse and Demanding Processing Applications The LabRAM II™ is built to handle diverse and demanding processing applications with a high degree of control and consistency. Its acoustic mixing technology allows for intense yet low-shear blending, making it suitable for sensitive materials while still achieving rapid, uniform results. Designed with flexibility in mind, it supports a wide range of vessel types, processing conditions, and optional accessories to meet evolving development needs. Beyond its core capabilities, the LabRAM II™ is designed to streamline workflows and improve process reliability. Its integrated human-machine interface (RAMWare) simplifies operation, while built-in data management tools support documentation and optimization. The system’s ability to scale directly to larger RAM platforms ensures that processes developed at the lab level can transition to production without added complexity or increased processing time. Key Processing Capabilities - Processes 2.2 lb (1 kg) per batch - Handles solids, powders, liquids, gases, and viscous materials - Supports milling, grinding, sieving, and coating (spray or dry) - Enables temperature control from -40°F (-40°C) to 392°F (200°C) (optional) - Offers vacuum processing down to 10 Torr (optional) - Process data download for analysis, documentation, and compliance reporting - Stores up to 100 recipes for repeatable operations Key Advantages - 10–100x faster processing compared to traditional mixers - Highly repeatable results for consistent product quality - Direct scalability across the RAM product line - Exceptional ingredient distribution - Erase cross contamination concerns and eliminate cleaning. - Process previously unmixable ingredients - Used worldwide in 40+ countries at 100's of universities, fortune 500 companies, governments and national laboratories. Specifications General Model LabRAM II Technology ResonantAcoustic® Mixing Intended Use Batch Mixing of Non-Hazardous Materials Unit Dimensions 33” H x 29” W x 24.5” D (cm: 83.8 x 73.7 x 62.2) Unit Weight 260 lb (117.9 kg) Country of Origin USA Certifications CE, UL Operating Specifications Maximum Payload Capacity 2.2 lb (1 kg) Compatible Materials Solids, Liquids, Pastes, High Viscosity Max Vessel Acceleration 100g at approximately 60 Hz Max Operating db < 80 db at 3’ Included Vessel Holder Assembly 2.5” - 5” H x 5” Diameter Included Vessels Application Specific Control Specifications Human Machine Interface Full Color Touch Screen Operating System RAMWare™ Programable Mix Recipe Storage Yes Remote Operation Optional Control Features Up to 100 stored recipes, live monitoring, acceleration control Power Specifications Required Voltage 100-120 / 200-240 VAC 1 Phase (50-60 Hz) The Most Capable Bench-Scale Mixer Ever The LabRAM II™ is Resodyn's flagship bench-scale ResonantAcoustic® Mixer — a full-featured, digitally controlled mixing and processing system built for laboratories and development environments that demand speed, precision, and the gentlest possible treatment of sensitive materials. With a payload capacity of up to 2.2 lbs (1 kg) and acceleration up to 100 g at 60 Hz, the LabRAM II delivers intense, bladeless, non-contact mixing across the widest range of materials available in any bench-top mixer: dry powders, liquids, slurries, pastes, and high-viscosity materials up to and beyond 10 million cP. No impellers. No shear damage. No compromises. Why the LabRAM II? Speed. RAM technology achieves thorough homogenization in minutes — 10× to 100× faster than conventional impeller methods for comparable blend quality. Quality. Uniform, distributed energy means no dead zones and no over-mixed regions. The result is a consistently superior blend, batch after batch. Safety. Sealed-vessel mixing eliminates exposure risk, cross-contamination, and the cleanup burden associated with impeller cleaning and validation. Scalability. Process parameters developed on the LabRAM II translate directly to larger RAM platforms — OmniRAM, RAM 5, RAM 55 — without requiring re-optimization. What you develop at the bench is what you produce at scale. Ideal For - Pharmaceutical API blending, wet granulation, and semi-solid compounding - Battery electrode slurry preparation - Cosmetic and personal care formulation - Polymer and advanced materials processing - Biological and cell-based compound processing - R&D and process development in any industry requiring low shear, high uniformity mixing "…[we] mix different rheologies with powder metals, highly viscous, and the LabRAM II has proven it can do that effectively. We're very impressed with the build quality of the mixer--it's a nice, solid, well-thought-out piece of equipment. It's done very well for us." -U.S. National Laboratory The LabRAM II is part of Resodyn's complete ResonantAcoustic® Mixer product family, which scales from the LabRAM I (500 g) through the production-scale RAM 55 (920+ lbs). All products are manufactured in Butte, Montana, USA, and operate in over 40 countries worldwide. For specifications, pricing, or to arrange a free demonstration using your materials, contact Resodyn Acoustic Mixers at info@resodynmixers.com or +1 (406) 497-5333. Direct RAM Scalability ResonantAcoustic® mixing scaled to your needs, from the lab to the production floor. LabRAM II FAQ What is the LabRAM II used for? The LabRAM II™ is used for high-performance laboratory mixing and processing of a wide range of materials, including powders, liquids, and viscous substances, making it ideal for formulation development and pilot-scale production. What types of materials can the LabRAM II process? The LabRAM II is designed to handle a very wide range of materials. Its key processing capabilities include mixing and processing any combination of solids/powders (from nano-scale and up), liquids/gases, and viscous/slurry materials, as well as coating, milling, and grinding processes. More specifically, RAM technology can efficiently mix virtually any combination of materials, processing them at nearly any particle size or behavior. Whether cohesive, agglomerated, nano-scale, or temperature-sensitive, a RAM mixer can control temperatures, apply vacuum, dry or spray-coat one particle on another, and effectively process any combination of powders, liquids, and high-viscosity materials. This includes liquids, pastes, and powders ranging from nano sizes to large particles, as well as highly viscous materials. In summary, the labRAM II lab mixer can process: - Solids & Powders — from nano-scale particles up to large particle sizes - Liquids & Gases - Viscous & Slurry materials - Cohesive or agglomerated materials - Temperature-sensitive materials (with temperature monitoring and control) - Pastes It can also perform coating, milling, and grinding processes, and optionally operate under vacuum for additional processing flexibility. What is the maximum batch capacity of the LabRAM II? The standard capacity is rated at 2.2 lb (1 kg). But this is not the whole story. Capacity is affected by the material itself and its rheological properties, by the acceleration at which you are processing, and even the weight of your container. Your capacity could be significantly higher or lower than 2.2 lb (1 kg). Speak to your sales representative about your material and schedule a mix test for an accurate capacity based on your application details. How does acoustic mixing differ from traditional mixing methods? Acoustic mixing is the proven method of superior mixing and processing. It is bladeless, and is driven by vertical oscillation of the mix vessel at ~60 Hz and acceleration up to 100 g. Because the machine operates at resonance, it is energy efficient. The high energy motion drives mixing energy throughout the mix vessel for rapid and homogenous results beyond what conventional mixing can achieve. Traditional mixing methods vary, but generally rely on spinning paddles, tumbling vessels, or kneading action. Each method has significant limitations due to uneven energy distribution, excessive heat generation, slow processing, and material segregation. Simple mixing applications may achieve a suitable result, but the advanced processing needs commonly found in energetics, pharmaceuticals, advanced materials, batteries, additive manufacturing, and complex chemistries are often underserved by traditional mixing and processing methods. RAM is the processing technology that repeatedly solves the most difficult mixing, milling, coating, and chemical reaction challenges. Can processes developed on the LabRAM II be scaled to larger production systems? Yes, Resodyn Mixers has developed an entire line of mixers from lab scale to production. What applications and industries are currently using a LabRAM II? Industries of all kinds are discovering the many benefits of RAM technology including, pharmaceutical, battery and energy storage, energetics, aerospace, cosmetics, adhesives and sealants, mechanochemistry, additive manufacturing, sintered materials, electronics, ceramics, lubricants and many other specialty materials.
CATEGORY
The LabRAM II™ is a high-performance acoustic mixer designed to bridge the gap between laboratory development and mid-scale production. Engineered for speed, precision, and flexibility, it delivers efficient, highly repeatable mixing across a wide range of materials, from powders and liquids to viscous slurries. The machine can process 2.2 lb (1 kg). With an intuitive touchscreen interface, robust data tracking, and scalable processing capabilities, the LabRAM II™ enables faster formulation development while maintaining consistency from lab to production. Need a custom solution? All mixers can be customized for unique automations and applications. Built for Diverse and Demanding Processing Applications The LabRAM II™ is built to handle diverse and demanding processing applications with a high degree of control and consistency. Its acoustic mixing technology allows for intense yet low-shear blending, making it suitable for sensitive materials while still achieving rapid, uniform results. Designed with flexibility in mind, it supports a wide range of vessel types, processing conditions, and optional accessories to meet evolving development needs. Beyond its core capabilities, the LabRAM II™ is designed to streamline workflows and improve process reliability. Its integrated human-machine interface (RAMWare) simplifies operation, while built-in data management tools support documentation and optimization. The system’s ability to scale directly to larger RAM platforms ensures that processes developed at the lab level can transition to production without added complexity or increased processing time. Key Processing Capabilities - Processes 2.2 lb (1 kg) per batch - Handles solids, powders, liquids, gases, and viscous materials - Supports milling, grinding, sieving, and coating (spray or dry) - Enables temperature control from -40°F (-40°C) to 392°F (200°C) (optional) - Offers vacuum processing down to 10 Torr (optional) - Process data download for analysis, documentation, and compliance reporting - Stores up to 100 recipes for repeatable operations Key Advantages - 10–100x faster processing compared to traditional mixers - Highly repeatable results for consistent product quality - Direct scalability across the RAM product line - Exceptional ingredient distribution - Erase cross contamination concerns and eliminate cleaning. - Process previously unmixable ingredients - Used worldwide in 40+ countries at 100's of universities, fortune 500 companies, governments and national laboratories. Specifications General Model LabRAM II Technology ResonantAcoustic® Mixing Intended Use Batch Mixing of Non-Hazardous Materials Unit Dimensions 33” H x 29” W x 24.5” D (cm: 83.8 x 73.7 x 62.2) Unit Weight 260 lb (117.9 kg) Country of Origin USA Certifications CE, UL Operating Specifications Maximum Payload Capacity 2.2 lb (1 kg) Compatible Materials Solids, Liquids, Pastes, High Viscosity Max Vessel Acceleration 100g at approximately 60 Hz Max Operating db< 80 db at 3’ Included Vessel Holder Assembly 2.5” - 5” H x 5” Diameter Included Vessels Application Specific Control Specifications Human Machine Interface Full Color Touch Screen Operating System RAMWare™ Programable Mix Recipe Storage Yes Remote Operation Optional Control Features Up to 100 stored recipes, live monitoring, acceleration control Power Specifications Required Voltage 100-120 / 200-240 VAC 1 Phase (50-60 Hz) Documents - LabRAM II Laboratory Mixer Product Data Sheet - LabRAM II User Manual The Most Capable Bench-Scale Mixer Ever The LabRAM II™ is Resodyn's flagship bench-scale ResonantAcoustic® Mixer — a full-featured, digitally controlled mixing and processing system built for laboratories and development environments that demand speed, precision, and the gentlest possible treatment of sensitive materials. With a payload capacity of up to 2.2 lbs (1 kg) and acceleration up to 100 g at 60 Hz, the LabRAM II delivers intense, bladeless, non-contact mixing across the widest range of materials available in any bench-top mixer: dry powders, liquids, slurries, pastes, and high-viscosity materials up to and beyond 10 million cP. No impellers. No shear damage. No compromises. Why the LabRAM II? Speed. RAM technology achieves thorough homogenization in minutes — 10× to 100× faster than conventional impeller methods for comparable blend quality. Quality. Uniform, distributed energy means no dead zones and no over-mixed regions. The result is a consistently superior blend, batch after batch. Safety. Sealed-vessel mixing eliminates exposure risk, cross-contamination, and the cleanup burden associated with impeller cleaning and validation. Scalability. Process parameters developed on the LabRAM II translate directly to larger RAM platforms — OmniRAM, RAM 5, RAM 55 — without requiring re-optimization. What you develop at the bench is what you produce at scale. Ideal For - Pharmaceutical API blending, wet granulation, and semi-solid compounding - Battery electrode slurry preparation - Cosmetic and personal care formulation - Polymer and advanced materials processing - Biological and cell-based compound processing - R&D and process development in any industry requiring low shear, high uniformity mixing "…[we] mix different rheologies with powder metals, highly viscous, and the LabRAM II has proven it can do that effectively. We're very impressed with the build quality of the mixer--it's a nice, solid, well-thought-out piece of equipment. It's done very well for us." -U.S. National Laboratory The LabRAM II is part of Resodyn's complete ResonantAcoustic® Mixer product family, which scales from the LabRAM I (500 g) through the production-scale RAM 55 (920+ lbs). All products are manufactured in Butte, Montana, USA, and operate in over 40 countries worldwide. For specifications, pricing, or to arrange a free demonstration using your materials, contact Resodyn Acoustic Mixers at info@resodynmixers.com or +1 (406) 497-5333. Powerful controls available through intuitive LCD touchscreen Rear view of mixer showing power connection, temp and vacuum control ports FAQ What is the LabRAM II used for? The LabRAM II™ is used for high-performance laboratory mixing and processing of a wide range of materials, including powders, liquids, and viscous substances, making it ideal for formulation development and pilot-scale production. What types of materials can the LabRAM II process? The LabRAM II is designed to handle a very wide range of materials. Its key processing capabilities include mixing and processing any combination of solids/powders (from nano-scale and up), liquids/gases, and viscous/slurry materials, as well as coating, milling, and grinding processes. More specifically, RAM technology can efficiently mix virtually any combination of materials, processing them at nearly any particle size or behavior. Whether cohesive, agglomerated, nano-scale, or temperature-sensitive, a RAM mixer can control temperatures, apply vacuum, dry or spray-coat one particle on another, and effectively process any combination of powders, liquids, and high-viscosity materials. This includes liquids, pastes, and powders ranging from nano sizes to large particles, as well as highly viscous materials. In summary, the labRAM II lab mixer can process: - Solids & Powders— from nano-scale particles up to large particle sizes - Liquids & Gases - Viscous & Slurry materials - Cohesive or agglomerated materials - Temperature-sensitive materials (with temperature monitoring and control) - Pastes It can also perform coating, milling, and grinding processes, and optionally operate under vacuum for additional processing flexibility. What is the maximum batch capacity of the LabRAM II? The standard capacity is rated at 2.2 lb (1 kg). But this is not the whole story. Capacity is affected by the material itself and its rheological properties, by the acceleration at which you are processing, and even the weight of your container. Your capacity could be significantly higher or lower than 2.2 lb (1 kg). Speak to your sales representative about your material and schedule a mix test for an accurate capacity based on your application details. How does acoustic mixing differ from traditional mixing methods? Acoustic mixing is the proven method of superior mixing and processing. It is bladeless, and is driven by vertical oscillation of the mix vessel at ~60 Hz and acceleration up to 100 g. Because the machine operates at resonance, it is energy efficient. The high energy motion drives mixing energy throughout the mix vessel for rapid and homogenous results beyond what conventional mixing can achieve. Traditional mixing methods vary, but generally rely on spinning paddles, tumbling vessels, or kneading action. Each method has significant limitations due to uneven energy distribution, excessive heat generation, slow processing, and material segregation. Simple mixing applications may achieve a suitable result, but the advanced processing needs commonly found in energetics, pharmaceuticals, advanced materials, batteries, additive manufacturing, and complex chemistries are often underserved by traditional mixing and processing methods. RAM is the processing technology that repeatedly solves the most difficult mixing, milling, coating, and chemical reaction challenges. Can processes developed on the LabRAM II be scaled to larger production systems? Yes, Resodyn Mixers has developed an entire line of mixers from lab scale to production. What applications and industries are currently using a LabRAM II? Industries of all kinds are discovering the many benefits of RAM technology including, pharmaceutical, battery and energy storage, energetics, aerospace, cosmetics, adhesives and sealants, mechanochemistry, additive manufacturing, sintered materials, electronics, ceramics, lubricants and many other specialty materials.
CATEGORY
The OmniRAM™ is Resodyn's first production scale acoustic mixer, capable of processing 11 lb (5 kg). It's designed to provide world-class ResonantAcoustic® Mixing (RAM) performance while bridging the gap between the LabRAM II's 1 kg bench-scale capacity and the RAM5's 36 kg production system. It represents a critical step in Resodyn's seamless scale-up pathway — delivering the same industry-leading RAM technology at a capacity and footprint ready for real-world production environments. Need a custom solution? All mixers can be customized for unique automations and applications. The Bridge From Bench to Production The OmniRAM's capacity of 11 lb (5 kg) is designed for larger than bench-scale development, pilot and small-scale production. With the ability to accept larger vessels, new scales are possible. The onboard system can retain 100 recipes, allowing for the rapid transition between different processes and products. Designed for floor operation, the unit is 75’’ wide and 35’’ deep. The work area is 42’’ off the ground, higher when vessels are used. Key Processing Capabilities - Processes up to 11 lb (5 kg) per batch - Handles solids, powders, liquids, gases, and viscous materials - Supports milling, grinding, sieving, and coating (spray or dry) - Enables temperature control from -15.8°F (-9°C) to 194°F (90°C) (optional) - Offers vacuum processing down to 10 Torr (optional) - Provides real-time monitoring and downloadable data for analysis - Stores up to 100 recipes for repeatable operations Key Advantages - 10–100x faster processing compared to traditional mixers - Highly repeatable results for consistent product quality - Direct scalability across the RAM product line - Exceptional ingredient distribution - Proven performance across global industries and applications - Housing and enclosure materials are sealed and purged Specifications General Model OmniRAM Technology ResonantAcoustic® Mixing Intended Use Batch Mixing of Non-Hazardous Materials Unit Dimensions 70″ H x 75″ W x 35″ D (cm: 106.7 x 190.5 x 88.9) Unit Weight 3,200 lb (1,451 kg) Country of Origin USA Certifications CE, UL, CFR 21 Part 11 Operating Specifications Maximum Payload Capacity 11 lb (5 kg) Compatible Materials Solids, Liquids, Pastes, High Viscosity Max Vessel Acceleration 100g at approximately 60 Hz Max Operating db < 80 db at 3’ Included Vessel Holder Assembly Application Specific Included Vessels Application Specific Control Specifications Human Machine Interface Full Color Touch Screen Operating System RAMWare™ Programable Mix Recipe Storage Yes Data Logging Yes Remote Operation Optional Control Features Up to 100 stored recipes, live monitoring, acceleration control Power Specifications Required Voltage 220-240 VAC/1 Phase (50-60 Hz) Documents - OmniRAM Product Data Sheet - OmniRAM Installation Manual Accessories The OmniRAM can be configured to your exact specifications and needs. The Bridge Between Lab Precision and Production Scale Uncompromising Mixing Performance The OmniRAM can process materials faster, better, more efficiently, and more productively, with customers trusting the core RAM technology for mixing of powders, liquids, gases, and viscous materials at higher quality and lower cost than many traditional mixing technologies. Operating as a non-contact, bladeless system, it eliminates contamination risks, reduces cleanup time, and ensures batch-to-batch repeatability — all hallmarks of Resodyn's ResonantAcoustic® platform. Advanced Control & Security The OmniRAM's onboard operating system provides machine operations control, recipe development and storage, as well as multiple level digital security and access control from operator to supervisor level. Vacuum and jacketed accessories are also available to increase processing capabilities, eliminating cross-contamination and cleanup while processing virtually any type of material. The jacketed vessel allows for mixing vessel temperatures ranging from 302°F (150°C) down to 34°F (1.1°C), giving operators precise thermal control throughout the process. Trusted by World-Class Customers The OmniRAM serves customers across advanced materials, pharmaceuticals, chemicals, and defense. Resodyn has worked with demanding customers such as NASA, multiple U.S. military agencies, well-known pharmaceutical manufacturers, top defense contractors, national laboratories, and advanced battery producers — all of whom rely on RAM technology to achieve results that simply aren't possible with conventional mixing equipment. The OmniRAM is where bench-scale discovery becomes production-scale reality — proudly engineered and manufactured in Butte, Montana. OmniRAM FAQ What is the OmniRAM used for? The OmniRAM is used for high-performance mixing and processing of a wide range of materials, making it ideal for production. What types of materials can the OmniRAM process? It can mix any combination of solids and powders (from nano-scale and up), liquids and gases, and viscous and slurry materials. It also has milling, grinding, sieving, and coating capabilities. What is the maximum batch capacity of the OmniRAM?? The standard capacity is rated at 11 lb (5 kg) but this is not the whole story. Capacity is affected by the material itself and its rheological properties, by the acceleration at which you are processing, and even the weight of your container. Your capacity could be significantly higher or lower than 11 lb (5 kg). The continuous version obviously changes that. Speak to your sales representative about your material and schedule a mix test for an accurate capacity based on your application details. How does acoustic mixing differ from traditional mixing methods? Acoustic mixing is the proven method of superior mixing. It is bladeless, and is driven by vertical oscillation of the mix vessel at ~60 Hz and acceleration up to 100 g. Because the machine operates at resonance, it is energy efficient. The high energy motion drives mixing energy throughout the mix vessel for rapid and homogenous results beyond what conventional mixing can achieve. Traditional mixing methods vary, but generally rely on spinning paddles, tumbling vessels, or kneading action. Each method has significant limitations due to uneven energy distribution, excessive heat generation, slow processing, and material segregation. Simple mixing applications may achieve a suitable result, but the advanced processing needs commonly found in energetics, pharmaceuticals, advanced materials, batteries, additive manufacturing, and complex chemistries are often underserved by traditional mixing and processing methods. RAM is the processing technology that repeatedly solves the most difficult mixing, milling, coating, and chemical reaction challenges. What options are there for an OmniRAM? Vacuum, temperature, various certifications
CATEGORY
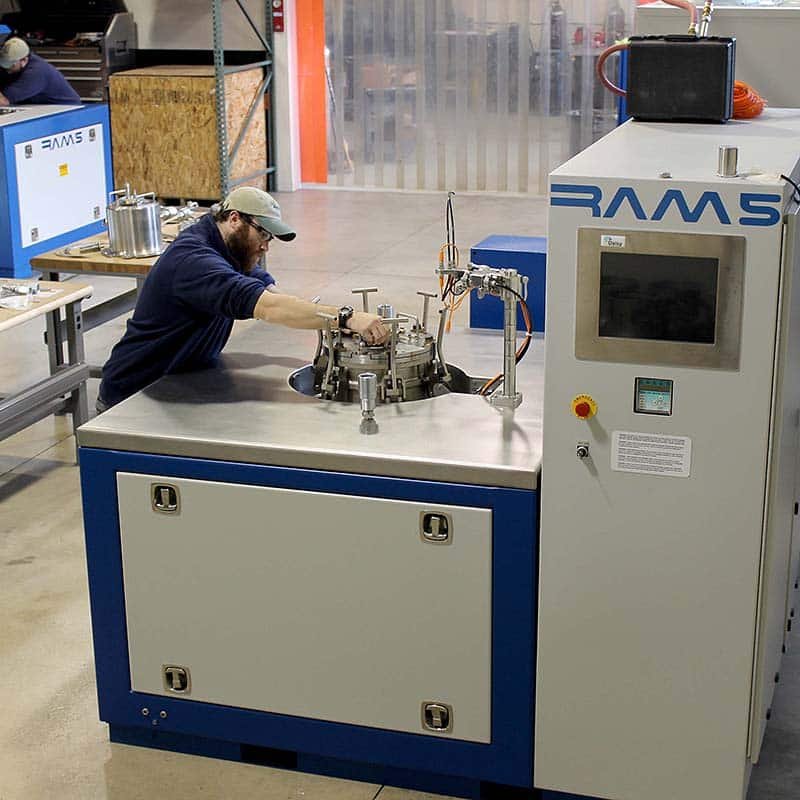
The Power of RAM at Production Scale Resodyn Acoustic Mixers' most popular production scale mixer, the RAM 5, drastically increases the productivity and capabilities of customers, enabling the manufacture of a broad range of products for less cost, more efficiently, more consistently, and more uniformly. It mixes without impellers and is capable of mixing up to 80 pounds (36 kg) of material. The RAM 5 is the only non-invasive mixer capable of mixing over 10 kg of materials with viscosities beyond 10 million cP. Need a custom solution? All mixers can be customized for unique automations and applications. The system provides onboard control of processing accessories, mixing vessel temperature control from 302°F (150°C) heating to 32°F (0°C) cooling, automatic or manual vacuum reaching 10 Torr, real-time monitoring of mixing parameters, and the ability to develop, store, and secure up to 100 recipes for permanent recording of operations and measured results. The RAM5 is ideal for full-scale production. Both on-board and remote operation allows for a variety of options. These controls extend to the optional temperature and vacuum systems. The temperature control is from 302 degrees F (150 degrees C) to 0 degrees F (-18 degrees C), while the vacuum can go as low as 10 Torr. It can use a variety of vessels, including most five-gallon plastic buckets. Key Processing Capabilities - Processes up to 80 lb (36 kg) per batch - Handles solids, powders, liquids, gases, and viscous materials - Supports milling, grinding, sieving, and coating (spray or dry) - Enables temperature control - Offers vacuum processing - Provides real-time monitoring and downloadable data for analysis - Stores up to 100 recipes for repeatable operations Key Advantages - 10–100x faster processing compared to traditional mixers - Highly repeatable results for consistent product quality - Direct scalability across the RAM product line - Exceptional ingredient distribution - Proven performance across global industries and applications Specifications General Model RAM5 Technology ResonantAcoustic® Mixing Intended Use Batch Mixing of Non-Hazardous Materials Unit Dimensions 72'' H x 80'' W x 60'' D (182.9cm x 203.2cm x 154.2 cm) Unit Weight 8,000 lb (3629 kg) Country of Origin USA Certifications CE, Others Operating Specifications Maximum Payload Capacity 80 lb or 5 gallons (36 kg or 21 L) Compatible Materials Solids, Liquids, Pastes, High Viscosity Max Vessel Acceleration 100g at approximately 60 Hz Max Operating db < 70 db at 3’ Included Vessel Holder Assembly Application Specific Included Vessels Application Specific Control Specifications Human Machine Interface Full Color Touch Screen Operating System RAMWare™ Programable Mix Recipe Storage Yes Data Logging Yes Remote Operation Optional Control Features Up to 100 stored recipes, live monitoring, acceleration control Power Specifications Required Voltage 460 VAC / 3 Phase Documents - RAM 5 Product Data Sheet Accessories The RAM5 production mixer will configured to your teams exact specifications. - Vacuum Control - Jacketed Vessel - Machine Chiller RAM 5™ by Resodyn Acoustic Mixers Production Scale ResonantAcoustic® Mixing — Up to 80 lb (36 kg) Since its introduction to the marketplace in 2007, RAM mixers have become the technology of choice for many commercial mixing and processing applications, with proven successful deployment from laboratories to production facilities at hundreds of locations worldwide, many in Fortune 500 companies. The RAM 5 represents the point where Resodyn's revolutionary ResonantAcoustic® technology truly steps into industrial-scale production. Mix-in-Case & Vessel Flexibility One of the RAM 5's most powerful and strategically important capabilities is its support for mix-in-case production. Because the RAM 5 is a non-invasive mixer, mixing can be done in sealed vessels of varying sizes and designs, and it can accommodate disposable or end-use vessels such as 6-gallon steel drums. This means materials — including energetics, advanced composites, and high-viscosity formulations — can be mixed directly in their final shipping or deployment container, eliminating hazardous transfer steps, reducing handling risk, cutting waste, and delivering enormous cost savings across the production lifecycle. The technology allows for considerable flexibility in the size and design of the vessel used for mixing, meaning batch mixes can be easily scaled from lab-scale quantities up to pilot and production mix amounts. RAM technology is well suited for mixing powder-powder blends, liquids, slurries, and viscous materials. Seamless Scale-Up RAM technology delivers direct scaling from bench to production levels with minimal or no adjustments in parameters or timing — meaning formulations developed on a LabRAM or OmniRAM translate directly to the RAM 5 without costly reformulation or requalification. The RAM 5 is also compatible with Resodyn's Continuous Acoustic Mixing (CAM) technology, enabling non-stop throughput for high-demand production environments. Compare the RAM family ResonantAcoustic® mixing scaled to your needs, from the lab to the production floor. RAM5 FAQ What is the RAM5 used for? The RAM5 is used for high-performance mixing and processing of a wide range of materials, making it ideal for large-scale production. What types of materials can the RAM5 process? The RAM5 is designed to handle a very wide range of materials. Its key processing capabilities include mixing and processing any combination of solids/powders (from nano-scale and up), liquids/gases, and viscous/slurry materials, as well as coating, milling, and grinding processes. More specifically, RAM technology can efficiently mix virtually any combination of materials, processing them at nearly any particle size or behavior. Whether cohesive, agglomerated, nano-scale, or temperature-sensitive, a RAM mixer can control temperatures, apply vacuum, dry or spray-coat one particle on another, and effectively process any combination of powders, liquids, and high-viscosity materials. This includes liquids, pastes, and powders ranging from nano sizes to large particles, as well as highly viscous materials. In summary, the RAM5 can process: - Solids & Powders — from nano-scale particles up to large particle sizes - Liquids & Gases - Viscous & Slurry materials - Cohesive or agglomerated materials - Temperature-sensitive materials (with temperature monitoring and control) - Pastes It can also perform coating, milling, and grinding processes, and optionally operate under vacuum for additional processing flexibility. What is the maximum batch capacity of the RAM5? The standard capacity is rated at 80 lbs (36 kg). But this is not the whole story. Capacity is affected by the material itself and its rheological properties, by the acceleration at which you are processing, and even the weight of your container. Your capacity could be significantly higher or lower than 80 lbs (36 kg). Speak to your sales engineer about your material and schedule a mix test for an accurate capacity based on your application and material details. How does acoustic mixing differ from traditional mixing methods? Acoustic mixing is the proven method of superior mixing and processing. It is bladeless, and is driven by vertical oscillation of the mix vessel at ~60 Hz and acceleration up to 100 g. Because the machine operates at resonance, it is energy efficient. The high energy motion drives mixing energy throughout the mix vessel for rapid and homogenous results beyond what conventional mixing can achieve. Traditional mixing methods vary, but generally rely on spinning paddles, tumbling vessels, or kneading action. Each method has significant limitations due to uneven energy distribution, excessive heat generation, slow processing, and material segregation. Simple mixing applications may achieve a suitable result, but the advanced processing needs commonly found in energetics, pharmaceuticals, advanced materials, batteries, additive manufacturing, and complex chemistries are often underserved by traditional mixing and processing methods. RAM is the processing technology that repeatedly solves the most difficult mixing, milling, coating, and chemical reaction challenges. What options are there for a RAM5? Vacuum, temperature, various certifications
CATEGORY
