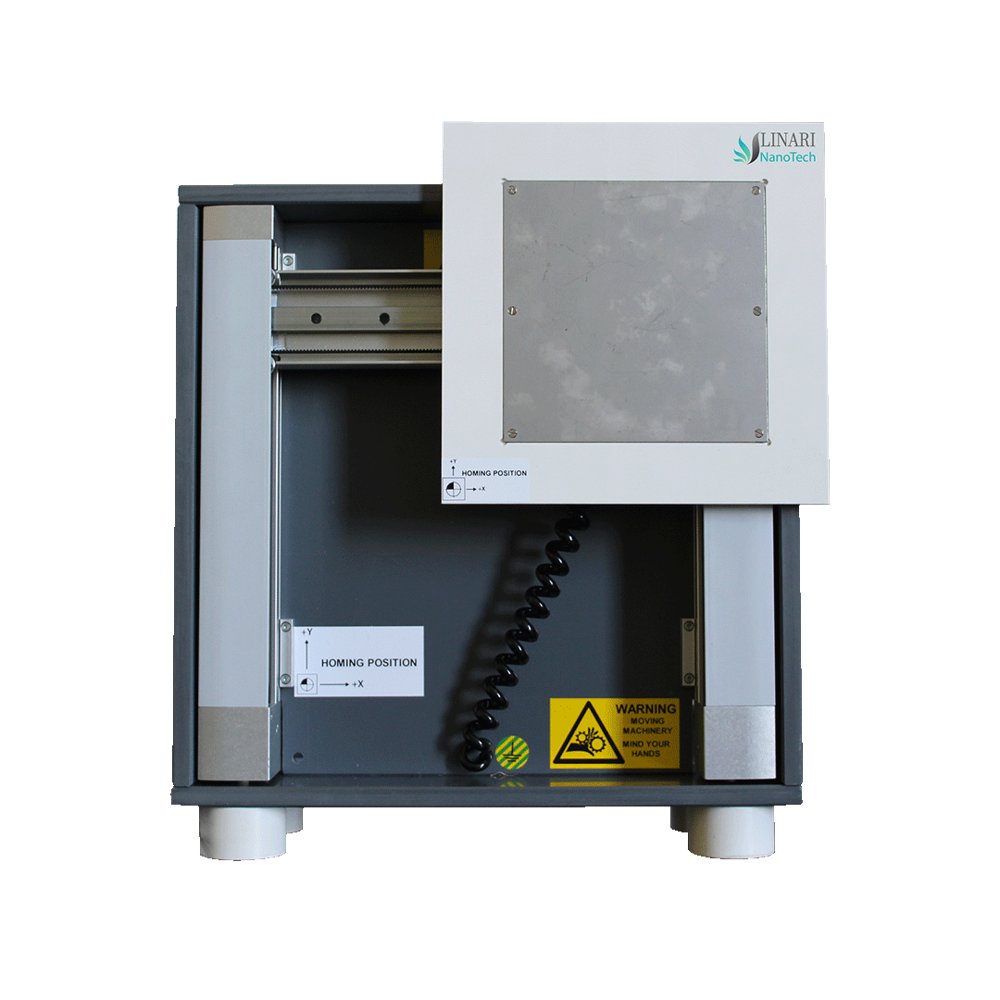
Our 2D Spin is the ideal machine for electrospinning applications, it can be combined with melt electrospinning and bioprinting systems. The perfect machine for creating super precise scaffolds or nanofibers. THE PERFECT MELT ELECTROSPINNING PRINTER FOR YOUR APPLICATIONS Compact machine, easy to install and ready to use. Plate collector configurable in vertical or horizontal position according to your needs. WHAT KIND OF FIBERS DO YOU GET WITH THIS MACHINE? With this XY table, you can deposit in an extremely precise way fibers with uniform thickness. WHAT ADVANTAGES DO YOU GET FROM USING THIS MACHINE? Thanks to the G-code interpreter you'll be able to draw the desired trajectory of the table through CAD software. This specificity is a prerogative of our machine. The CSV interpreter allows you to create work programs in a simple way through spreadsheets. Writing with fibers, not just spraying them Conventional electrospinning deposits fibers where the electric field takes them. With an XY table under G-code control you decide the path: the emitter follows a trajectory drawn in CAD, with a repetition accuracy of ±0.02 mm and scanning speed up to 500 mm/s over a 460×460 mm work space. That precision opens up applications ordinary electrospinning cannot reach: - Melt electrospinning writing (MEW) - with the heating needle system up to 250 °C, deposit solvent-free fibers along defined paths to build lattice scaffolds layer by layer. - Patterned scaffolds - defined pore geometry and fiber orientation, instead of a random mat. - Uniform coatings on large plates - programmed coverage of the full collector area, without thick centres and thin edges. - Bioprinting integration - the table can be combined with bioprinting systems for hybrid constructs. Up to 2000 work programs can be stored in internal memory and transferred over Web or FTP, so a validated recipe is reproduced identically every time. 2D Spin is the XY motion stage: the high voltage generator is not included. POWER SUPPLY - Voltage line: 110/230 V ac. - Frequency: HZ 50/60. - Nominal current: 10 A. - Motor type: Stepper motor. - Interfaces: 3,5'' LCD color touch screen, Web, FTP for transfer of work programs. - Emergency stop: yes. DIMENSIONS CONTROL UNIT - Length: 550 mm. - Width: 300 mm. - Height: 550 mm. DIMENSION MOTION UNIT - Length: 410 mm. - Width: 360 mm. - Height: 154 mm. - Work space Length: 460 mm. - Work space Width: 460 mm. - Weight max: 11 kg PLATE COLLECTOR UNIT - Max travel lenght: 190 mm. - Max emitter distance: 190 mm. - Scanning speed: 500 mm/s. - Repetition accuracy: ±0.02 mm. NEEDLE SUPPORT CONFIGURATION - Max travel lenght X: 190 mm. - Max emitter distance Y: 190 mm. - Scanning speed: 500 mm/s. - Adjustable spinning distance between needle and collector: 40...230 mm. - Manual adjustable direction Z: up to 160 mm. - Repetition accuracy: ±0.02 mm. OTHER FEATURES - Recipes files: saving up to 2000 work programs in internal memory. - CSV interpreter: the CSV interpreter allows you to create work programs in a simple and powerful way through spreadsheets. - GCODE interpreter: G-code interpreter you can draw the desired trajectory through a CAD software and send the work program to the device. OPTIONAL FEATURES - Machine 3 D Spin: add a rotary axis movement to create 3D structures. - Heating needle system: for melt electrospinning up to 250°C. Is a high voltage generator included? No. 2D Spin is the XY motion stage and the generator must be added separately. If you prefer a system that arrives complete and ready to run, the Gantry 3D Spin includes the 40 kV generator, station hood, syringe pump, rotation unit, needles and collectors. How precise is the deposition? Repetition accuracy is ±0.02 mm on both the plate collector unit and the needle support, with scanning speed up to 500 mm/s and a work space of 460×460 mm. How do I program a trajectory? Two ways: draw the path in CAD and send it as G-code, or build the work program in a spreadsheet and load it as CSV. Up to 2000 programs can be stored in internal memory and transferred over Web or FTP. Can I use it for melt electrospinning writing? Yes. With the heating needle system up to 250 °C you can deposit solvent-free fibers along programmed paths, which is the basis of melt electrospinning writing for lattice scaffolds. Can I adjust the needle-to-collector distance? Yes. The spinning distance is adjustable between 40 and 230 mm, with a manual Z adjustment up to 160 mm - useful when a longer flight path is needed for solvent evaporation. Can I add a rotary axis later? Yes. Adding rotary axis movement for 3D structures is what turns this setup into the Gantry 3D Spin configuration. Can the plate collector be used vertically? Yes. The plate collector can be configured in vertical or horizontal position according to your setup.
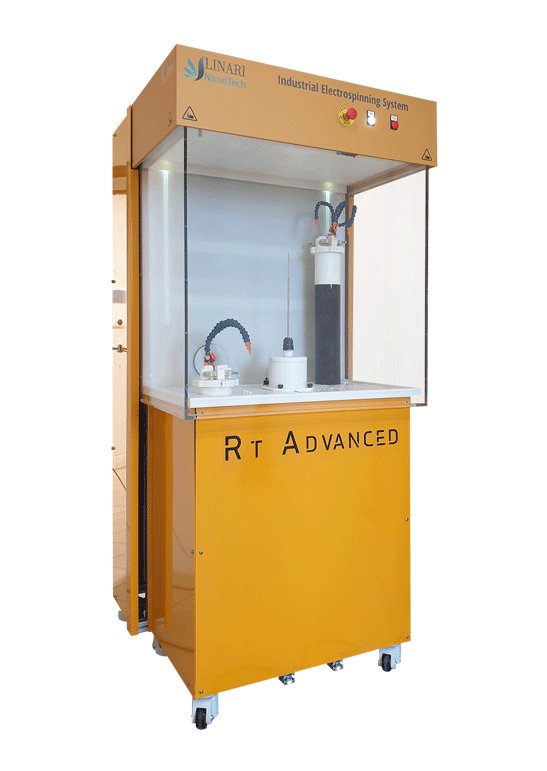
RT Advanced is a 60 kV industrial electrospinning system for unattended multi-material production: two fully independent spinning groups, up to 8 pumps, closed-loop thickness control, an electrically insulated chamber, climate control precise to 10–70% RH ±2% and ambient–50 °C ±1 °C, and an audit trail designed to meet 21 CFR Part 11. It is built for laboratories and companies that need to move from experiments to repeatable production — including production that has to stand up to an audit. Two independent groups, one on each side of the collector RT Advanced is not one spinning station with more pumps bolted on. It is two complete, fully independent groups, each with its own 60 kV generator, its own four pumps, its own automatic needle cleaning and its own blow spinning system. The two groups sit symmetrically about the collector axis, and the collector itself acts as an electrostatic shield between them. That is what makes the architecture work: multi-emitter systems normally fight themselves, because jets repel each other and the field distorts. With the collector in the middle, each group works against a controlled potential rather than against the other group, and interference is minimised by geometry rather than corrected afterwards. Practically, it means the left side and the right side can run different materials, at different voltages, with different gas flows, depositing onto the same collector in a single run. Built for regulated environments Most electrospinning systems are research instruments. RT Advanced ships with the documentation set required to qualify the machine in a regulated production environment, and with the software controls an auditor expects to find. - Named user accounts with role-based access. Every action is attributed to a person, not to a shared login. - A complete audit trail, designed to meet 21 CFR Part 11. Parameter changes, run start and stop, alarms and interventions are recorded with user, timestamp and electronic signature — supporting pharmaceutical audits on both sides of the Atlantic. - Alarms sent by email as they occur, so an out-of-range parameter or a fault does not go unnoticed between visits. - Full process telemetry. Voltage, flow rates, gas flow, chamber temperature and humidity, collector speed and measured thickness are logged for every run. - Qualification documentation for regulated environments, available on request. Your process data stays yours RT Advanced complies with the EU Data Act: you get free, secure, programmatic access to the machine’s configuration and telemetry data, and you can move it wherever you need — a cloud platform or a server inside your own network. Connectivity is built on Alleantia technology and supports more than ten integration protocols, so batch records and process data live in your systems rather than locked inside ours. For a validated process, that is the difference between a machine you can integrate and one you have to work around. The machine stops when the target is reached One or more laser sensors measure the deposit on the rotating collector in several positions while the run is in progress. RT Advanced does not just display that number — it acts on it: deposition continues until the target thickness is reached, then the machine stops on its own. Measuring in more than one position along the collector also tells you whether the deposit is uniform, not only how thick it is at one point. Fibres are too soft and thin for calipers or micrometers, so this is the only practical way to control thickness while the process runs. Eight materials, one deposit, no operator With eight independent programmable pumps across the two groups you can build structures no single-station system can reach: multilayer membranes, gradient scaffolds, blended mats, and core-shell fibers with coaxial needles. No competing system offers eight. Three features let it run overnight and over the weekend without anyone standing by: - Automatic needle cleaning with timed jets of compressed gas, on each group. A clogged needle is the most common cause of an interrupted run. - Closed-loop thickness control, so the run ends at the target rather than when someone comes back. - Controlled atmosphere — temperature, humidity and inert gas flushing keep the process identical from the first hour to the last. In case of blackout or malfunction the system interrupts production automatically. Blow spinning, digitally controlled, on both groups An optional blow spinning module adds a gas flow that helps draw the jet. It raises throughput, and it lets you process solutions that will not open under electric field alone — more viscous, less conductive, or in solvent systems that resist electrospinning. It also runs with the high voltage off, as pure solution blow spinning. That is not a variant of the same process: it is a second technology on the same machine, and it covers polymers that electrospinning cannot handle at all. There is one blow spinning system per group, so the two sides can run different gas flows on different materials in the same run — or one side in electrospinning and the other in blow spinning. Gas flow is set digitally and measured with a Coriolis flow meter, which reads mass flow rather than volume — so the reading is unaffected by pressure and temperature, and the same setting gives the same result in January and in July. Most hybrid systems use a float meter and a hand valve. Because the flow is a digital parameter, it belongs to the recipe and to the telemetry, like voltage or solution flow rate. No tubes, no dead volume, no cross-contamination The collector stays fixed while the syringes move on the vertical axis. RT Advanced is the only system that moves the syringes without using tubes, and that has three consequences that matter in a regulated process: nothing is left behind in a tube between runs, there is no dead volume when you change material, and cross-contamination between materials is structurally prevented rather than managed by cleaning. It also means almost no solution is wasted at each material change — which matters when the polymer is expensive or available in milligrams. From a single sample to continuous production Flat or drum collectors from 1 to 250 mm in diameter and up to 500 mm long are replaced quickly thanks to a single-piece carrier. The collector rotates on a vertical axis, clockwise or anticlockwise, up to 5000 rpm without oscillation — which is what makes tubular structures with aligned fibres possible. The collector is insulated from ground and can be biased with its own generator when the process calls for it. For continuous output, a vertical-axis continuous belt produces flat substrates tens of metres long in a single run. Climate control, configured to your process Humidity is the parameter that most often makes a recipe work in one season and fail in another, and different processes need it controlled in different directions. Our external air treatment unit (UTA) connects directly to RT Advanced and is configured around your process: vaporisers when humidity has to be added, a chiller when it has to be removed, plus heating, heating and cooling, or drying stages as required. In its full configuration the UTA holds relative humidity between 10 and 70% to within 2% and temperature from ambient up to 50 °C to within 1 °C. What sets it apart is not those numbers on their own — it is holding them while extracting solvent vapour. Most systems treat the two as alternatives: either you seal the chamber to stabilise the climate, or you ventilate it and lose control of humidity. The UTA does both, with a controlled airflow strong enough to prevent solvent stagnation and gentle enough not to drag the nanofibres off the collector. You keep a stable process, a safe atmosphere and the fibres you produced. An insulated chamber, because grounded metal steals fibres The entire internal surface of the chamber is made from electrically insulating materials. Competing systems use metal components and structures which, by construction, have to be earthed — and earthed metal near a high voltage field attracts nanofibres continuously. Those fibres are lost yield: they never reach the collector, and their absence changes what does. Insulating the chamber removes that loss at the source rather than compensating for it, which is why the same solution yields more usable material per run and a more consistent deposit. Pumps that work at 60 kV, continuously In RT Advanced the syringes themselves sit at high potential and the pumps operate safely and continuously at up to 60,000 V — as far as we know, the highest figure available on the market for needle-based electrospinning systems. This is what makes it possible to move the syringes with the needles instead of feeding them through tubes, and it widens the range of polymers and solvent systems you can process, since the field is no longer the limiting factor. A thermal map, not just a set-point What a set-point does not tell you is how uniform the temperature is around the collector, where the fibres actually form — a region you cannot easily instrument without disturbing the process. So we modelled it: finite element analysis of the chamber shows the temperature distribution around the vertical collector, and the deposition volume sits in a uniform region. We share the analysis on request. The simulation is an analysis, not a measurement, and we do not present it as one. It is how we designed the airflow, and it is why we can explain — rather than assert — why results stay consistent along the collector. Support that keeps you compliant - Warranty extensions up to five years. - Scheduled maintenance plans, designed to support your own regulatory obligations rather than only to fix faults. - A dedicated remote assistance module, so most process and control issues are resolved without waiting for a visit. - Direct access to our R&D team in Pisa — the people who built the machine. Technical specifications - Two fully independent spinning groups, symmetrically placed about the collector axis, which acts as an electrostatic shield. - One 60 kV high voltage generator per group. - Four pumps per group — up to 8 independent syringes in total. - Automatic needle cleaning with timed jets of compressed gas, on each group. - Optional blow spinning module, one per group: digital gas flow control with Coriolis mass flow measurement; operates with or without high voltage. - Multi-needle or coaxial needle system. - Flat or drum collectors, 1 to 250 mm in diameter, maximum length 500 mm. - Collector rotation clockwise or anticlockwise, vertical axis up to 5000 rpm. - Collector insulated from ground, connectable to its own high voltage generator. - Continuous belt for flat substrates up to tens of metres. - External air treatment unit (UTA) with vaporisers, chiller, heating, heating/cooling and drying stages configured to the process. - UTA full configuration: 10–70% RH ±2%, ambient to 50 °C ±1 °C, with simultaneous solvent extraction. - Inert gas flushing. - Chamber internal surfaces in electrically insulating materials — no earthed metal attracting fibres. - Syringe pumps operating continuously at up to 60 kV. - Closed-loop thickness control with one or more laser sensors (optional). - Built-in suction system. - Access and visibility on three sides of the spinning chamber. - Industrial tablet-PC with WiFi control. - Omron industrial components for the control electronics. General | Unit | Value | Note Depth | mm | 1035 Height | mm | 2200 Width | mm | 1050 Total weight | kg | 400 | approx. Max power consumption | kW | 1.5 – 4 | depending on options installed Supply voltage | V AC | 230 | single phase 50-60 Hz High voltage generators | 2 × 60 kV | one per spinning group Ventilation system | Yes Humidity control | % RH | 10 – 70 | ±2%, UTA full configuration Temperature control | °C | ambient – 50 | ±1 °C, UTA full configuration Warranty | 1 year | extensions available up to 5 years Safety - Opening of the spinning chamber is blocked when high voltage is present. - Automatic interruption of production in case of blackout or malfunction. - Active control system to eliminate sparks and high voltage discharges. Producing medical devices in a cleanroom? A dedicated version of RT Advanced is available for medical device manufacturing: washable stainless steel external structures, automatic mandrels inside the chamber, and an anthropomorphic robotic arm outside, so scaffolds and grafts are produced in a fully automated, clean island. Geometries are customised to the application. Options: Syringe Pumps on primary HV; Secondary HV Generator+ Pumps; Environmental control system; Collector; Laser Measuring System (10 nm) for online real-time thickness control with sliding holder +/- 40mm Shipping date: 20 Oct
CATEGORY
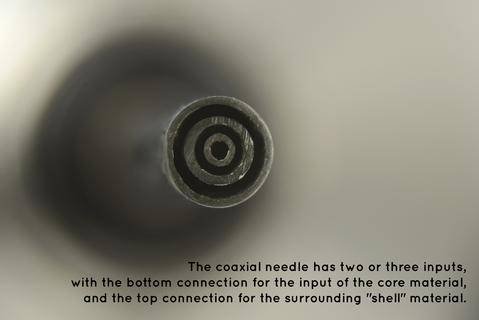
Our Sealed Coaxial Needle Kit is the ideal solution for core-shell electrospinning with any type of polymer, even in the most corrosive solvents — a complete, ready-to-use set at an accessible price. SUITABLE FOR CORE-SHELL ELECTROSPINNING All our needles are manufactured in AISI 316 stainless steel and assembled entirely by a laser welding process. Thanks to the manufacturing material, it is possible to spin any type of polymer at temperatures up to 120 °C in the standard configuration. WHAT ADVANTAGES DO YOU GET FROM USING THIS KIT? With coaxial needles you gain the ability to spin two or more polymers simultaneously within the same fiber, producing fibers with an inner core and outer shell. This is useful when a single material would force a compromise between two properties — for example, one material offers the desired mechanical strength, while a different material shows a better degradation rate. Two standard versions are available, with two or three concentric layers, customizable upon request. These needles are very compact and make it possible to create high-productivity configurations: they can be assembled in parallel up to tens of units thanks to a simple, solid mechanical structure and the distribution of solutions through Luer-UNF connections. The rear threaded hole permits both fastening to the support structure and a stable connection of the high voltage. LOOKING FOR A MORE VERSATILE SOLUTION? In our Modular Coaxial Needle Kit, every concentric needle is independent, so it can be equipped with a different diameter and supplied with solutions of different materials through standard Luer Lock connections. PRODUCTS INCLUDED - Sealed Coaxial Needles (2 or 3 layers) - Dielectric Support - Luer-UNF Fittings: 2 pcs (2 layers) / 3 pcs (3 layers) STANDARD DIMENSIONS Inner needle: G21 - OD: 0.83 mm - ID: 0.51 mm Middle needle: G15 - OD: 1.83 mm - ID: 1.37 mm Outer needle: G11 - OD: 3.05 mm - ID: 2.39 mm COMPATIBILITY It can be integrated on machines that have a number of syringe pumps equal to the number of layers used. FREQUENTLY ASKED QUESTIONS What is the difference between this kit and the Modular Coaxial Needle Kit? This kit uses laser-welded sealed needles with fixed geometry (G21/G15/G11) — compact, robust and significantly more affordable. The modular kit offers interchangeable tips and full disassembly, at a higher price. If you are starting with core-shell electrospinning, this sealed kit is the most cost-effective entry point. Can I use this kit with a non-Linari electrospinning system? Yes. The needles connect through standard Luer-UNF fittings and the dielectric support is free-standing, so the kit works with any electrospinning setup that has one syringe pump per layer and a high-voltage supply. Is everything I need included? The kit includes the sealed coaxial needle, the dielectric support and the Luer-UNF fittings. You additionally need syringes, Luer Lock tubing and your electrospinning system with pumps and high-voltage supply.
CATEGORY
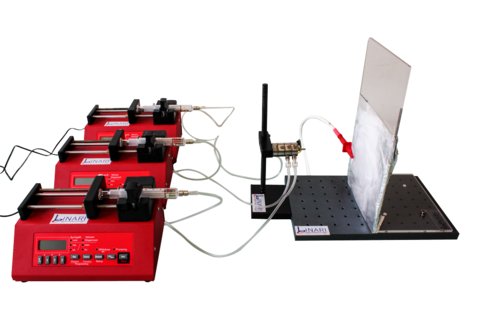
The Modular Coaxial Needle Kit is the ideal solution for core-shell electrospinning with any type of polymer, even in the most corrosive solvents. Removable and interchangeable tips, easy to clean. IDEAL FOR CORE-SHELL ELECTROSPINNING The modular coaxial needles are made of AISI 316 stainless steel and can be manufactured with tips of different diameters, even beyond the catalog range. Thanks to their stable and accurate structure they can also operate at high temperatures (up to 120 °C) without geometric deformation or leakage of liquids or gas. The minimum configuration requires 2 concentric layers, which can be disassembled or integrated at any time with a third external layer. WHAT ADVANTAGES DO YOU GET FROM USING THIS KIT? Every concentric needle is independent, so it can be equipped with a different diameter and supplied with solutions of different materials through standard Luer Lock connections. All surfaces are designed without dead spaces for easy cleaning. The screw closing system guarantees great simplicity of maintenance. The perfect axial-symmetrical shape — guaranteed by the exclusive design with all fluid connections behind the needle plane — and the perfectly smooth surface of the coaxial needles ensure an electric field of excellent quality for stable and accurate nanofiber production even in difficult conditions. WHY PREFER A MODULAR COAXIAL SYSTEM INSTEAD OF A SEALED ONE? With coaxial needles you gain the ability to spin two or more polymers simultaneously within the same fiber, producing a fiber with an inner core and outer shell. This is useful when a single material would force a compromise between two properties — for example, one material offers the desired mechanical strength, while a different material shows a better degradation rate. Compared to the Sealed Coaxial Needle Kit, this modular solution allows changing tips according to your needs, making it a long-lasting investment. WHICH SYSTEMS IS IT COMPATIBLE WITH? The modular coaxial needles can be integrated with the Starter Kit, the RT Collector, the Easy Drum and the RT Advanced, provided the system has a number of syringe pumps equal to the number of concentric layers used. WHICH PRODUCTS ARE INCLUDED? DOUBLE LAYER COAXIAL NEEDLES WITH ADJUSTABLE DIELECTRIC SUPPORT Base of modular coaxial needle, layer 1 – internal: 1 pc. Base of modular coaxial needle, layer 2 – intermediate: 1 pc. Tip, layer 1, gauge 21 (0.83 mm): 1 pc. Tip, layer 2, gauge 15 (1.83 mm): 1 pc. Dielectric support for coaxial needles: 1 pc. Sealing kit for coaxial needles: 1 pc. Female Luer adapter: 2 pcs. TRIPLE LAYER COAXIAL NEEDLES WITH ADJUSTABLE DIELECTRIC SUPPORT AND LUER POWER CONNECTORS Base of modular coaxial needle, layer 1 – internal: 1 pc. Base of modular coaxial needle, layer 2 – intermediate: 1 pc. Base of modular coaxial needle, layer 3 – external: 1 pc. Tip, layer 1, gauge 21 (0.83 mm): 1 pc. Tip, layer 2, gauge 15 (1.83 mm): 1 pc. Tip, layer 3, gauge 11 (3.05 mm): 1 pc. Dielectric support for coaxial needles: 1 pc. Sealing kit for coaxial needles: 1 pc. Luer-UNF adapter: 3 pcs. WATCH THE VIDEO TO FIND OUT HOW TO ASSEMBLE IT SEE VIDEO DISCOVER THE COAXIAL ACCESSORIES BROCHURE FREQUENTLY ASKED QUESTIONS Should I choose the 2-layer or 3-layer kit? Choose the 2-layer kit for standard core-shell fibers (one core, one shell). The 3-layer kit adds an external layer for triaxial fibers — useful for multi-drug delivery systems, protective intermediate layers or complex release profiles. You can also start with 2 layers and add the third later. What equipment do I need to use this kit? An electrospinning system with one syringe pump per layer (2 or 3 pumps) and a high-voltage supply. The kit is compatible with all Linari systems (Starter Kit, RT Collector, Easy Drum, RT Advanced) and with third-party setups via standard Luer Lock connections. How does it differ from the sealed coaxial needles? Sealed coaxial needles are compact welded units with fixed geometry, ideal for parallel high-productivity arrays. The modular kit costs more but offers interchangeable tips, full disassembly for cleaning, and diameter changes at any time.
CATEGORY
Base of modular coaxial needle to customize your coaxial electrospinning equipment. The ideal solution for core-shell electrospinning with any type of polymer, even in the most corrosive solvents. SETUP WITH INTERCHANGEABLE AND DETACHABLE TIPS All the tips are made of AISI 316 stainless steel and are laser welded for maximum cleanliness and precision. Customized tips can be created upon request with diameters and lengths differing from those listed in this catalog. WHAT ADVANTAGES DO YOU GET FROM USING INTERCHANGEABLE TIPS? With coaxial needles, you gain the ability to spin two or more polymers simultaneously within the same fiber. This allows the production of fibers with an inner core and outer shell. The interchangeable tips make it easy to replace the tip of every layer of the coaxial needle in order to adapt different diameters. Assembly is done with a simple screwdriver, supplied as standard, thanks to a proprietary high-precision connection with the base, which makes it possible to achieve stable and repeatable geometries. DISCOVER HOW TO ASSEMBLE THE MODULAR COAXIAL NEEDLE LOOKING FOR AN ALL-INCLUSIVE SOLUTION? We offer the base, dielectric support, tips, sealing kit and female Luer adapter — all included in a single kit. COMPATIBLE TIP SIZES LENGTH 35.75 MM - COAX-N108: gauge 21 – 0.83 mm OD – 0.51 mm ID - COAX-N118: gauge 15 – 1.83 mm OD – 1.37 mm ID LENGTH 25.25 MM - COAX-N208: gauge 21 – 0.83 mm OD – 0.51 mm ID - COAX-N218: gauge 15 – 1.83 mm OD – 1.37 mm ID - COAX-N230: gauge 11 – 3.05 mm OD – 2.39 mm ID LENGTH 15 MM - COAX-N308: gauge 21 – 0.83 mm OD – 0.51 mm ID - COAX-N318: gauge 15 – 1.83 mm OD – 1.37 mm ID - COAX-N330: gauge 11 – 3.05 mm OD – 2.39 mm ID BASE SELECTION GUIDE LAYER 1 BASE – INTERNAL Suitable with all COAX-N tips. At least the second layer (COAX-L2M) is necessary to complete a coaxial system. LAYER 2 BASE – INTERMEDIATE - Layer 1 COAX-N108 → Layer 2 COAX-N218 - Layer 1 COAX-N118 → Layer 2 COAX-N230 At least the first layer (COAX-L1M) is necessary to complete a coaxial system. LAYER 3 BASE – EXTERNAL Layer 1 COAX-N108 → Layer 2 COAX-N218 → Layer 3 COAX-N330 The first (COAX-L1M) and second layer (COAX-L2M) are necessary to complete a coaxial system. FREQUENTLY ASKED QUESTIONS What do I need for a complete 2-layer modular coaxial needle? Two bases (Layer 1 internal + Layer 2 intermediate), two tips (e.g. gauge 21 + gauge 15), a dielectric support and a sealing kit. The Modular Coaxial Needle Kit includes everything at a bundle price. Can I upgrade from 2 to 3 layers later? Yes — that is the main advantage of the modular system. Add the Layer 3 external base and a gauge 11 tip at any time; the existing components remain in use. How do the modular bases differ from sealed coaxial needles? Modular bases accept interchangeable tips and can be disassembled for cleaning and diameter changes, while sealed coaxial needles are welded single pieces — more compact and lower cost, but with fixed geometry.
CATEGORY
