By Intelligent Enclosures Corp.
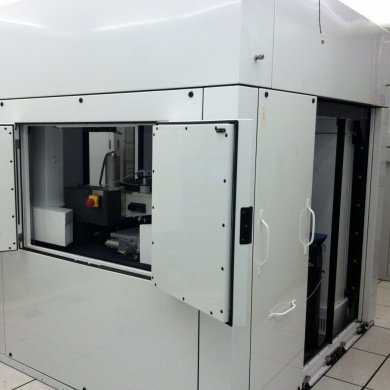
MiniEnvironments for Semiconductor applications for critical metrology processes. From Concept to Volume Production for Semiconductor MiniEnvironments Veeco wanted to create a leading edge Atomic Force Microscope (AFM) for semiconductor metrology with a resolution of 1 nanometer within an Class 1 in operation (ISO 14644-1), acoustically shielded, and temperature stabilized environment. Veeco chose Intelligent Enclosures to join Veeco’s team to engineer, design and prototype the required Enclosure. Working with Veeco and Veeco’s vibration isolation and stage suppliers iE engineered an airflow design using Computational Fluid Dynamics (CFD) analysis that would allow the AFM environment to meet Veeco’s goals while accommodating the required AFM architecture. Veeco contracted with iE to develop the industrial design for the Enclosure to support the market launch of the new Insight 3DAFM™ Tool at Semicon Tokyo. Then iE’s design staff created an Enclosure meeting the performance and design requirements and providing adequate access for maintenance, servicing, and user interface. Next iE manufactured prototype Enclosures for Veeco which iE integrated with the vibration isolation table and X-Y-Z wafer stage at iE’s facility. iE then tested for compliance to Veeco’s performance criteria. After the successful completion of the prototype phase, iE developed a production ready design for Veeco. iE was given the contract to build the production Enclosure and provide Veeco with integration services. iE receives from Veeco’s isolation table and stage vendors an assembled table and stage on which iE installs its pre-assembled Enclosure, mounts all the additional panels and components, and routes electrical cabling. iE tests the assembled Enclosure with the Tool in the operating condition for ISO Class 1 cleanliness, temperature stability, and acoustic attenuation. By shipping a fully integrated and tested system iE provides Veeco with reduced total cycle times, providing their Customers a much earlier delivery date. Final product Enclosure ready to ship Integration of Enclosure Enclosure integrated to stage Assembly of Enclosure Enclosure is assembled. Engineering and Design of Enclosure Enclosure is designed to meet specific needs.
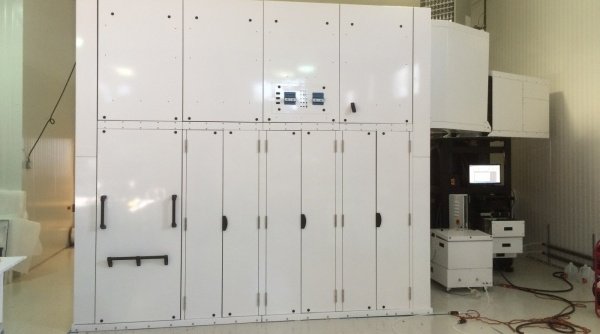
AFM Enclosure for NIST Surface and Nanostructure Metrology Group iE was contacted by Bruker-Nano to provide an Enclosure for a unique Atomic Force Microscope. This special AFM was designed for the Traceable Scanning Probe Nano Characterization project created by NIST’s Surface and Nanostructure Metrology Group. Building on iE’s previous experience with PGL, iE designed a custom Enclosure that provides better than 0.01 ºC temperature stability (± 3mK) at the AFM head allowing for extremely precise measurements by the AFM. The enclosure has removable insulated panels for ease of access and assembly. The Environmental Control Unit (ECU) composing of a fan impellor with an external motor, a TEHE (Thermal Electric Heat Exchanger) combined with a pump and coils, and onboard electronics was designed to fit within the envelope of the Enclosure and provide precisely controlled air to the process chamber below. CFD analysis was used to develop an airflow scheme that allowed for maximum temperature stability at the AFM head. An external control box with a GUI (Graphical User Interface) is provided for monitoring and adjusting the Enclosures performance. Along with facilities chilled water the GUI is attached to the onboard ECU.
CATEGORY
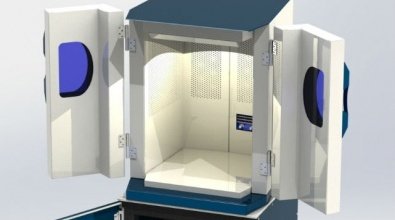
Most recently iE was contacted by a nanotechnology company for an Enclosure for a yet to be revealed project. In addition to.010ºC temperature stability control achieved by iE on the previous projects this new customer requested spatial uniformity across a 3m x 2m area of ±0.020ºC at the process height. iE designed a movable enclosure with a remote Environmental Control Unit containing a fan impellor with external motor, a TEHE with associated water pump and piping, and electrical components therefore removing those vibration and heat sources from the critical chamber. The movable enclosure allows for safe and easy assembly around the customer’s multi-ton custom instrument. Temperature stability and uniformity is monitored by an array of temperature probes placed in a grid at the ceiling diffuser level and is feed into iE’s control computer that then controls the output to iE’s TEHE providing.01ºC control to the air entering the chamber. To improve temperature uniformity across the 3m x 2m zone of interest iE developed a diffusion grid with a segmented re-heater system. NIST traceable probes with ±0.0005ºC accuracy placed at the process level provide temperature data which iE’s PAC uses to fine tune the air temperature for each region as the air moves through the individual diffusers/heater assemblies and the slightly cooler than setpoint air is re-heated by the diffusers. This arrangement of a iE’s typical precise temperature control via TEHE and water feed coils with a re-heat diffusion grid allowed iE to surpass the specification for ± 0.020ºC spatial uniformity, achieving a temperature spatial uniformity range of 0.019ºC during testing following installation at the customer facility around the instrument over the 3m x 2m critical area while achieving a temperature stability of ±0.0045ºC. In a smaller area of 3m x.5m the Enclosure provides a temperature spatial uniformity range of 0.012ºC and a temperature stability of ±0.0045ºC.
CATEGORY
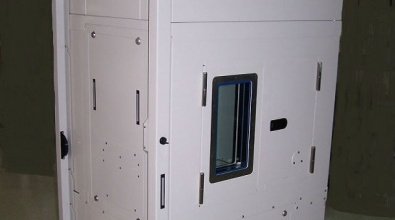
iE has designed and engineered Acoustic Enclosures for smaller instruments that are either floor mounted or table top designs. iE has developed an interlocking panel design that eliminates the need for a frame for the smaller enclosures allowing for quick and easy assembly around the instrument. The panels employ either a stainless steel construction for Semiconductor use or steel construction as an option for non-semiconductor instruments. For table top instruments, iE has designed enclosures which integrate vibration isolators into the table legs allowing for a smooth unified appearance. Acoustic enclosures can include such features as internal noise absorbing baffles with perforated metal skins and non-parallel side walls and ceiling to mitigate the incidences of standing waves. Bulkhead connectors and special thick rubber pass-through blocks are incorporated for passing facilities and data in and out from the instrument
CATEGORY
Today’s instruments require a low vibration environment to operate at a nanometer scale, thus many of the Enclosures designed and built by Intelligent Enclosures incorporate features to provide reduced acoustic noise levels as well as mitigate structural vibration. Whether for Mini-Environments for semiconductors applications with air systems and temperature control, or stand-alone Acoustic Enclosures for table top instruments, iE has successfully designed enclosures with very low internal acoustic noise levels.
CATEGORY
