By Resodyn Acoustic Mixers, Inc.
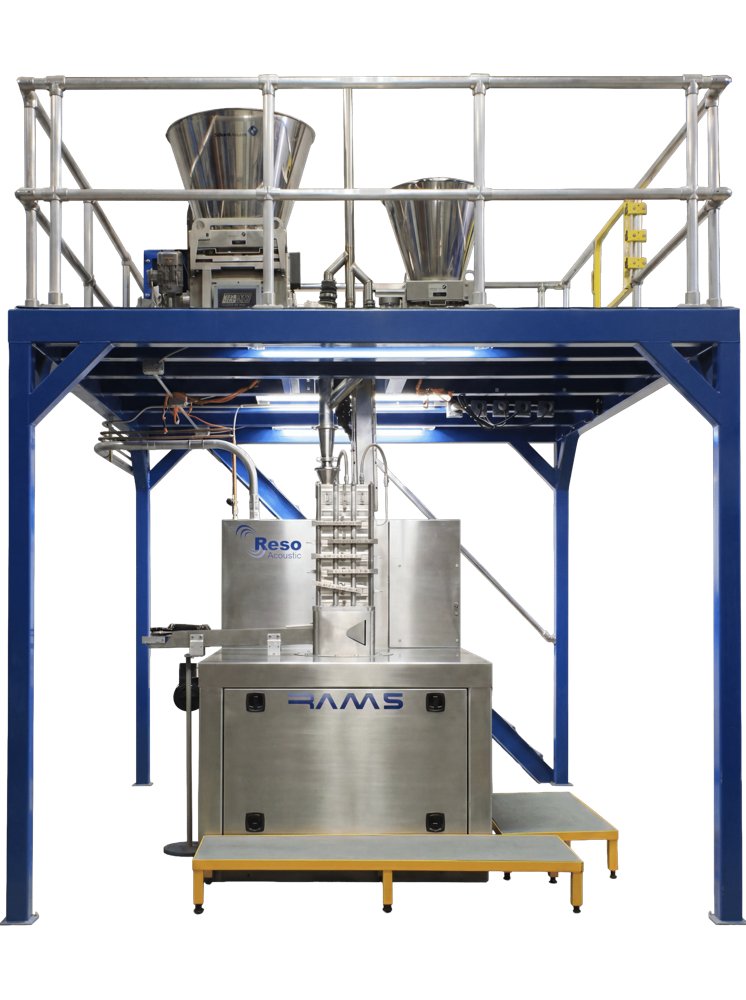
Resodyn Acoustic Mixers' production scale pharmaceutical mixer, the RAM5 Pharma Continuous, brings the awesome power of ResonantAcoustic® Mixing to larger scale to drastically increase productivity and expand capabilities. Built on flexible and universal processing capabilities, the RAM5 Pharma delivers exceptional RSD (Relative Standard Deviation) results, improved efficiency with rapid mixing and dispersion times, and new product opportunities at a larger payload capacity for RAM batch and continuous systems. Each RAM5 Pharma configuration matches the right processing functions with critical processing demands and exceeds the required performance beyond traditional technologies. Need a custom solution? All mixers can be customized for unique automations and applications. Pharmaceutical-Grade Performance at Production Scale The RAM 5 Pharma is purpose-built for pharmaceutical manufacturers who have outgrown bench-scale development and need the same mixing quality, content uniformity, and process reproducibility they saw in R&D. Since the RAM process is consistent across scales, the transition from R&D to production is seamless, unlike conventional mixing equipment. The RAM5 Pharma mixer creates enormous quantities of products. The flexibility of vessel size and shape allows for a rapid change in inputs and outputs. The enclosed structure allows for easy cleaning and sanitization. Key Processing Capabilities - Processes up to 80 lb (36 kg) per batch - Handles solids, powders, liquids, gases, and viscous materials - Supports milling, grinding, sieving, and coating (spray or dry) - Enables temperature control - Offers vacuum processing - Provides real-time monitoring and downloadable data for analysis - Stores up to 100 recipes for repeatable operations Key Advantages - 10–100x faster processing compared to traditional mixers - Highly repeatable results for consistent product quality - Direct scalability across the RAM product line - Exceptional ingredient distribution - Proven performance across global industries and applications - Variety of certifications available General Model RAM5 Pharma Technology ResonantAcoustic® Mixing Intended Use Batch Mixing of Pharmaceutical Materials Unit Dimensions 72'' H x 80'' W x 60'' D (182.9cm x 203.2cm x 154.2 cm) Unit Weight 8,000 lb (3629 kg) Country of Origin USA Certifications Available CE, UL, CFR 21 Part 11 Operating Specifications Maximum Payload Capacity 80 lb or 5 gallons (36 kg or 21 L) Compatible Materials Solids, Liquids, Pastes, High Viscosity Max Vessel Acceleration 100g at approximately 60 Hz Max Operating db < 70 db at 3’ Included Vessel Holder Assembly Application Specific Included Vessels Application Specific Control Specifications Human Machine Interface Full Color Touch Screen Operating System RAMWare™ Programable Mix Recipe Storage Yes Data Logging Yes Remote Operation Optional Control Features Up to 100 stored recipes, live monitoring, acceleration control Power Specifications Required Voltage 460 VAC / 3 Phase Documents - RAM5 Product Data Sheet Accessories The RAM5 Pharma will be configured exactly how you need. - Vacuum System - Jacketed Vessel System - Machine Chiller GMP and Contamination Free RAM uses vibrational energy instead of impellers or blades, and mixing occurs in sealed containers, minimizing cross-contamination, exposure risks, and reducing cleaning validation burdens — all crucial for GMP compliance. This bladeless, closed-system approach is not simply a convenience — for pharmaceutical manufacturers, it is a critical compliance and safety advantage that streamlines regulatory approval and reduces the time and cost associated with cleaning validation between product runs. RAM ensures uniform distribution of active pharmaceutical ingredients (APIs) even at low concentrations — such as below 1% — which helps maintain dose accuracy and content uniformity, critical for tablet and capsule formulations. Comprehensive Processing Capabilities Key processing capabilities include mixing and processing 80 lbs (36 kg) or more of any combination of solids and powders from nano-scale up, liquids and gases, and viscous and slurry materials, as well as coating, milling, and grinding processes, all with onboard control of processing accessories. The RAM5 Pharma is available with a full menu of processing options including temperature monitoring and control and mixing under vacuum. Standard functions include recipe development and retention, real-time parameter monitoring and recording, 100% processing data retention, multiple operator security levels, and multiple mixing vessel options. The system supports up to 80 lbs of mix capacity in extendable 5-gallon mixing vessels with application-specific vessel options. Proven in the World's Top Pharmaceutical Operations From the world's top pharmaceutical companies to international manufacturers and global tech giants, Resodyn Acoustic Mixer installations in over 40 countries are in use today, all sharing a single, powerful technology platform. The RAM5 Pharma represents that platform at its most powerful production-ready pharmaceutical configuration — delivering the speed, uniformity, and traceability demanded by modern drug manufacturing. Real-world impact is well documented. One pharmaceutical manufacturer reported challenges mixing a viscous, 10,000 cP solids-loaded transdermal cream consisting of water, excipient, API, and a sticky acrylate adhesive — a process that previously required multiple material addition steps and up to eight hours with an overhead stirrer. With a Resodyn RAM system, that mix was completed in just over two minutes. What is the RAM5 Pharma used for? The RAM5 Pharma Continuous is used for high-performance mixing and processing of a wide range of pharmaceutical materials, making it ideal for continuous large-scale production. What types of materials can the RAM5 Pharma process? The RAM 5 Pharma is designed to handle a very wide range of materials. Its key processing capabilities include mixing and processing any combination of solids/powders (from nano-scale and up), liquids/gases, and viscous/slurry materials, as well as coating, milling, and grinding processes. More specifically, RAM technology can efficiently mix virtually any combination of materials, processing them at nearly any particle size or behavior. Whether cohesive, agglomerated, nano-scale, or temperature-sensitive, a RAM mixer can control temperatures, apply vacuum, dry or spray-coat one particle on another, and effectively process any combination of powders, liquids, and high-viscosity materials. This includes liquids, pastes, and powders ranging from nano sizes to large particles, as well as highly viscous materials. In summary, the RAM 5 Pharma can process: - Solids & Powders — from nano-scale particles up to large particle sizes - Liquids & Gases - Viscous & Slurry materials - Cohesive or agglomerated materials - Temperature-sensitive materials (with temperature monitoring and control) - Pastes It can also perform coating, milling, and grinding processes, and optionally operate under vacuum for additional processing flexibility. What is the maximum batch capacity of the RAM5 Pharma? The standard capacity is rated at 80 lbs (36 kg). But this is not the whole story. Capacity is affected by the material itself and its rheological properties, by the acceleration at which you are processing, and even the weight of your container. Your capacity could be significantly higher or lower than 80 lbs (36 kg). Speak to your sales representative about your material and schedule a mix test for an accurate capacity based on your application details. How does acoustic mixing differ from traditional mixing methods? Acoustic mixing is the proven method of superior mixing and processing. It is bladeless, and is driven by vertical oscillation of the mix vessel at ~60 Hz and acceleration up to 100 g. Because the machine operates at resonance, it is energy efficient. The high energy motion drives mixing energy throughout the mix vessel for rapid and homogenous results beyond what conventional mixing can achieve. Traditional mixing methods vary, but generally rely on spinning paddles, tumbling vessels, or kneading action. Each method has significant limitations due to uneven energy distribution, excessive heat generation, slow processing, and material segregation. Simple mixing applications may achieve a suitable result, but the advanced processing needs commonly found in energetics, pharmaceuticals, advanced materials, batteries, additive manufacturing, and complex chemistries are often underserved by traditional mixing and processing methods. RAM is the processing technology that repeatedly solves the most difficult mixing, milling, coating, and chemical reaction challenges. What options are there for a RAM5 Pharma? Vacuum, temperature, various certifications
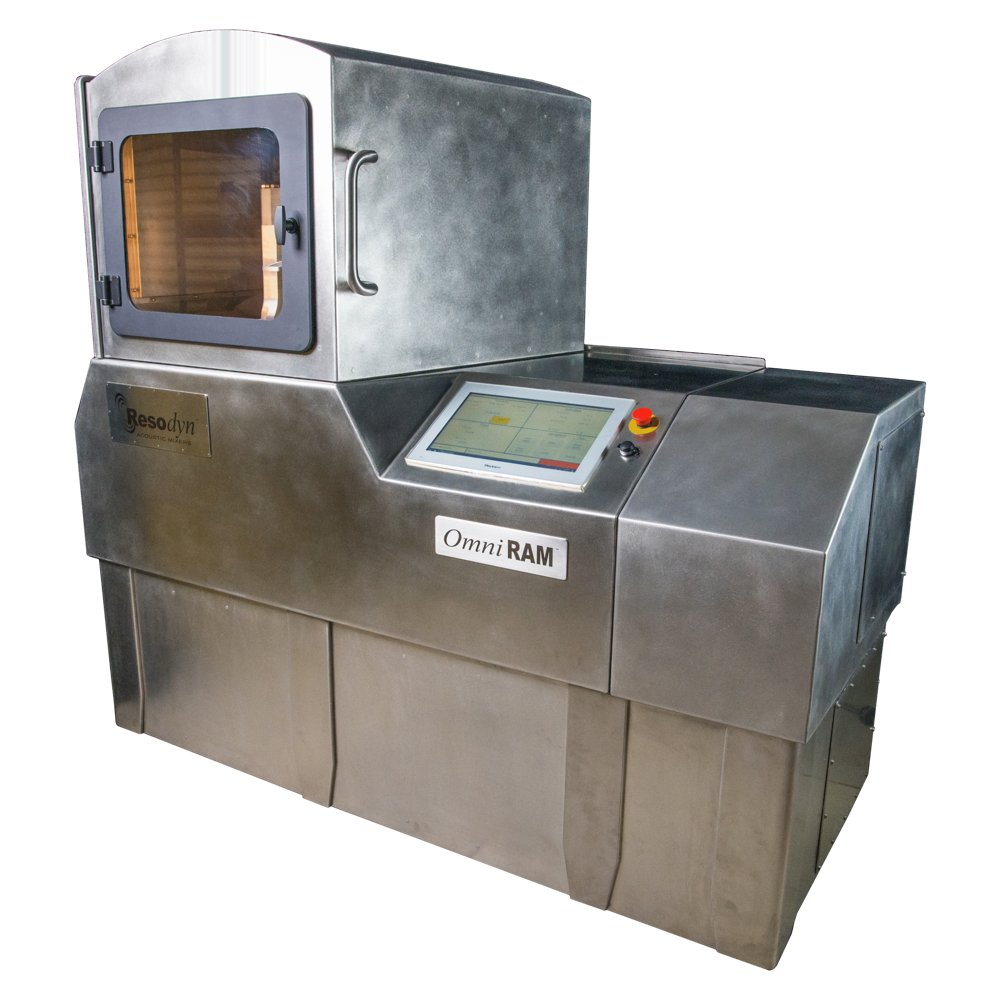
The OmniRAM Pharma delivers processing speed, mixing power, and optimal development on a mid-scale pilot and production scale. With an integrated touchscreen-controlled operating system, the OmniRAM Pharma enables recipe development, process and data management, with optional processing accessories including vacuum systems and temperature-controlled vessels. It delivers exceptional RSD, improved efficiency, and new product opportunities. Need a custom solution? All mixers can be customized for unique automations and applications. Full Spectrum Processing Capabilities Key processing capabilities include mixing and processing up to 11 lbs (5 kg) of any combination of solids and powders from nano-scale up, liquids and gases, viscous and slurry materials, along with coating, milling, and grinding processes. The OmniRAM Pharma is also adaptable to Resodyn's Continuous Acoustic Mixing (CAM) platform. Whether blending APIs with excipients, producing semi-solid topical formulations, dispersing nano-scale drug particles, or processing high-viscosity biologics, the OmniRAM Pharma handles it all — faster, cleaner, and more uniformly than conventional mixing technologies. The OmniRAM pharmaceutical mixer can combine significant amounts of API and excipients. This makes it perfect for research and small-scale production. A sliding hood provides protection from any spills or accidents. Optional temperature control from 302 degrees F (150 degrees C) and 0 degrees F (-18 degrees C) extends the possible products. The ability to use remote control allows for safer production. Key Processing Capabilities - Processes up to 11 lb (5 kg) per batch - Handles solids, powders, liquids, gases, and viscous materials - Supports milling, grinding, sieving, and coating (spray or dry) - Enables temperature control from -15.8°F (-9°C) to 194°F (90°C) (optional) - Offers vacuum processing down to 10 Torr (optional) - Provides real-time monitoring and downloadable data for analysis - Stores up to 100 recipes for repeatable operations Key Advantages - 10–100x faster processing compared to traditional mixers - Highly repeatable results for consistent product quality - Direct scalability across the RAM product line - Exceptional ingredient distribution - Proven performance across global industries and applications - Housing and enclosure materials are sealed and purged Specifications General Model OmniRAM Pharma Technology ResonantAcoustic® Mixing Intended Use Batch Mixing of Pharmaecutical Materials Unit Dimensions 70″ H x 75″ W x 35″ D (cm: 106.7 x 190.5 x 88.9) Unit Weight 3,200 lb (1,451 kg) Country of Origin USA Certifications CE, UL, CFR 21 Part 11 Operating Specifications Maximum Payload Capacity 11 lb (5 kg) Compatible Materials Solids, Liquids, Pastes, High Viscosity Max Vessel Acceleration 100g at approximately 60 Hz Max Operating db < 80 db at 3’ Included Vessel Holder Assembly Application Specific Included Vessels Application Specific Purge Air 65 psi 4.482 bars @ 150 SCFM (4246.5 l/min) Control Specifications Human Machine Interface Full Color Touch Screen Operating System RAMWare™ Programable Mix Recipe Storage Yes Data Logging Yes Remote Operation Optional Control Features Up to 100 stored recipes, live monitoring, acceleration control Power Specifications Required Voltage 220-240 VAC/1 Phase (50-60 Hz) Documents - OmniRAM Product Sheet - Uniformity in Pharmaceuticals: How RAM Equals Low RSD Accessories The OmniRAM Pharma will be configured to your exact specifications. - Vacuum System - Strobe Light - Jacketed Vessel System - Machine Chiller The Bridge Between Lab and Full Production In pharmaceutical development, the jump from bench-scale formulation to full commercial production has historically been one of the most difficult, costly, and time-consuming transitions in the entire drug development lifecycle. The OmniRAM Pharma is specifically designed to close that gap. With an 11 lb (5 kg) payload capacity, the OmniRAM Pharma is a full-featured, digitally controlled batch mixer for larger-than-bench-scale development, clinical trials, pre-production, and small-scale production and processing. This makes it the ideal pharmaceutical workhorse for organizations running Phase I and Phase II clinical trials, where batch sizes have outgrown the PharmaRAM II but full RAM 5 Pharma production volumes aren't yet required. The OmniRAM Pharma ensures that the formulation quality, content uniformity, and process parameters established during early R&D are preserved and validated at clinical scale — so there are no surprises when the time comes to move to full production. Built on the Same World-Class Platform The OmniRAM Pharma is built on the same technology platform and operating system as Resodyn's PharmaRAM II, supporting repetitive and precursor processes and including vacuum and temperature monitoring capability. This shared platform is a critical advantage — it means operators who have worked on the PharmaRAM II need no additional training, and process parameters developed on the bench translate directly and predictably to the OmniRAM Pharma without re-testing or reformulation. RAM technology scales easily without additional testing from development to pilot to production scales. GMP Compliance & Data Integrity Built In The OmniRAM Pharma's onboard operating system provides pharmaceutical manufacturers with the full suite of data management and security tools required for GMP-compliant operations. Recipe development, storage, and security ensure that every batch is produced to exactly the same validated parameters — a requirement for clinical trial material manufacturing and eventual regulatory submission. Real-time parameter monitoring and 100% processing data retention give quality assurance teams complete batch traceability from start to finish. RAM ensures uniform distribution of active pharmaceutical ingredients even at low concentrations — such as below 1% — helping maintain dose accuracy and content uniformity, which are critical for tablet and capsule formulations. For clinical trial material where dosing precision can directly affect patient outcomes and trial data integrity, this level of uniformity is not optional — it is essential. What is the OmniRAM Pharma used for? The OmniRAM Pharma is used for high-performance mixing and processing of a wide range of pharmaceutical materials, making it ideal for pilot and production. What types of materials can the OmniRAM Pharma process? The OmniRAM Pharma is designed to handle a very wide range of materials. Its key processing capabilities include mixing and processing any combination of solids/powders (from nano-scale and up), liquids/gases, and viscous/slurry materials, as well as coating, milling, and grinding processes. More specifically, RAM technology can efficiently mix virtually any combination of materials, processing them at nearly any particle size or behavior. Whether cohesive, agglomerated, nano-scale, or temperature-sensitive, a RAM mixer can control temperatures, apply vacuum, dry or spray-coat one particle on another, and effectively process any combination of powders, liquids, and high-viscosity materials. This includes liquids, pastes, and powders ranging from nano sizes to large particles, as well as highly viscous materials. In summary, the RAM 5 Pharma can process: - Solids & Powders — from nano-scale particles up to large particle sizes - Liquids & Gases - Viscous & Slurry materials - Cohesive or agglomerated materials - Temperature-sensitive materials (with temperature monitoring and control) - Pastes It can also perform coating, milling, and grinding processes, and optionally operate under vacuum for additional processing flexibility. What is the maximum batch capacity of the OmniRAM Pharma? The standard capacity is rated at 11 lb (5 kg). But this is not the whole story. Capacity is affected by the material itself and its rheological properties, by the acceleration at which you are processing, and even the weight of your container. Your capacity could be significantly higher or lower than 11 lb (5 kg). Speak to your sales representative about your material and schedule a mix test for an accurate capacity based on your application details. How does acoustic mixing differ from traditional mixing methods? Acoustic mixing is the proven method of superior mixing and processing. It is bladeless, and is driven by vertical oscillation of the mix vessel at ~60 Hz and acceleration up to 100 g. Because the machine operates at resonance, it is energy efficient. The high energy motion drives mixing energy throughout the mix vessel for rapid and homogenous results beyond what conventional mixing can achieve. Traditional mixing methods vary, but generally rely on spinning paddles, tumbling vessels, or kneading action. Each method has significant limitations due to uneven energy distribution, excessive heat generation, slow processing, and material segregation. Simple mixing applications may achieve a suitable result, but the advanced processing needs commonly found in energetics, pharmaceuticals, advanced materials, batteries, additive manufacturing, and complex chemistries are often underserved by traditional mixing and processing methods. RAM is the processing technology that repeatedly solves the most difficult mixing, milling, coating, and chemical reaction challenges. What options are there for an OmniRAM Pharma? Vacuum, temperature, various certifications
CATEGORY
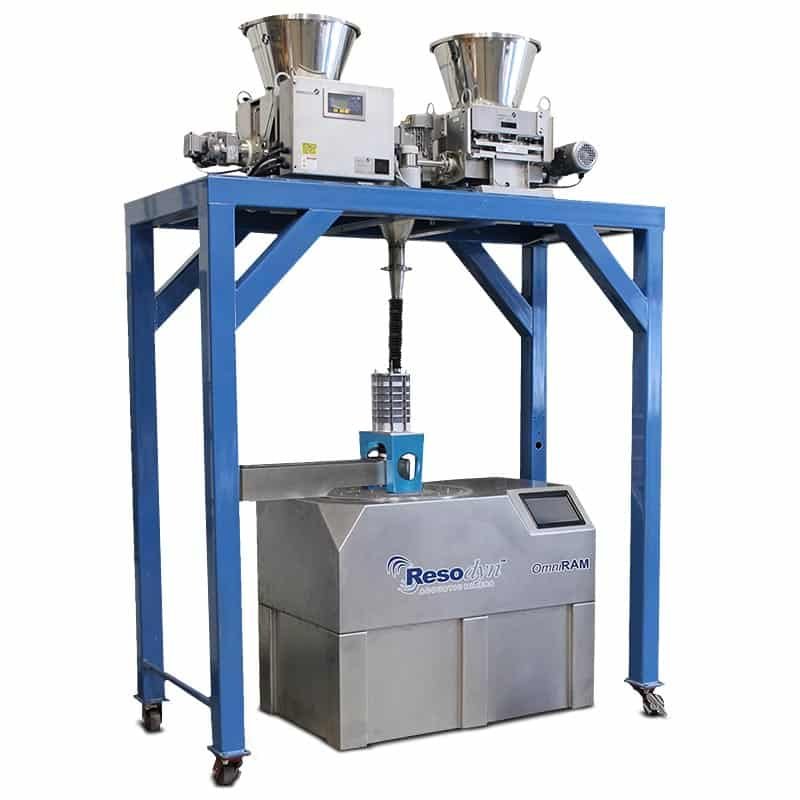
The OmniRAM Pharma's set of design and features reflects users' critical requirements, delivering processing speed, mixing power, and optimal parameter development to a mid-scale pilot and production RAM machine. With an integrated touchscreen-controlled operating system, the OmniRAM Pharma enables recipe development, process and data management, with optional processing accessories including vacuum systems and temperature-controlled vessels. The OmniRAM Pharma delivers exceptional RSD results, improved efficiency with rapid mixing and dispersion times, and new product opportunities at a payload capacity that bridges the PharmaRAM II's bench-scale developmental capabilities with larger RAM batch and continuous systems. Need a custom solution? All mixers can be customized for unique automations and applications. Full Spectrum Processing Capabilities Key processing capabilities include mixing and processing up to 11 lbs (5 kg) of any combination of solids and powders from nano-scale up, liquids and gases, viscous and slurry materials, along with coating, milling, and grinding processes. The OmniRAM Pharma is also adaptable to Resodyn's Continuous Acoustic Mixing (CAM) platform. Whether blending APIs with excipients, producing semi-solid topical formulations, dispersing nano-scale drug particles, or processing high-viscosity biologics, the OmniRAM Pharma handles it all — faster, cleaner, and more uniformly than conventional mixing technologies. The OmniRAM pharmaceutical mixer can combine significant amounts of API and excipients. This makes it perfect for research and small-scale production. A sliding hood provides protection from any spills or accidents. Optional temperature control from 302 degrees F (150 degrees C) and 0 degrees F (-18 degrees C) extends the possible products. The ability to use remote control allows for safer production. Key Processing Capabilities - Processes up to 11 lb (5 kg) per batch - Handles solids, powders, liquids, gases, and viscous materials - Supports milling, grinding, sieving, and coating (spray or dry) - Enables temperature control from -15.8°F (-9°C) to 194°F (90°C) (optional) - Offers vacuum processing down to 10 Torr (optional) - Provides real-time monitoring and downloadable data for analysis - Stores up to 100 recipes for repeatable operations Key Advantages - 10–100x faster processing compared to traditional mixers - Highly repeatable results for consistent product quality - Direct scalability across the RAM product line - Exceptional ingredient distribution - Proven performance across global industries and applications - Housing and enclosure materials are sealed and purged Specifications General Model OmniRAM Pharma Technology ResonantAcoustic® Mixing Intended Use Continuous Mixing of Pharmaceutical Materials Unit Dimensions 70″ H x 75″ W x 35″ D (cm: 106.7 x 190.5 x 88.9) Unit Weight 3,200 lb (1,451 kg) Country of Origin USA Certifications CE, UL, CFR 21 Part 11 Operating Specifications Maximum Payload Capacity 11 lb (5 kg) Compatible Materials Solids, Liquids, Pastes, High Viscosity Max Vessel Acceleration 100g at approximately 60 Hz Max Operating db < 80 db at 3’ Included Vessel Holder Assembly Application Specific Included Vessels Application Specific Purge Air 65 psi 4.482 bars @ 150 SCFM (4246.5 l/min) Control Specifications Human Machine Interface Full Color Touch Screen Operating System RAMWare™ Programable Mix Recipe Storage Yes Data Logging Yes Remote Operation Optional Control Features Up to 100 stored recipes, live monitoring, acceleration control Power Specifications Required Voltage 220-240 VAC/1 Phase (50-60 Hz) Documents - OmniRAM Product Sheet - Uniformity in Pharmaceuticals: How RAM Equals Low RSD Accessories The OmniRAM Pharma will be configured to your exact specifications. - Vacuum System - Strobe Light - Jacketed Vessel System - Machine Chiller The Bridge Between Lab and Full Production In pharmaceutical development, the jump from bench-scale formulation to full commercial production has historically been one of the most difficult, costly, and time-consuming transitions in the entire drug development lifecycle. The OmniRAM Pharma is specifically designed to close that gap. With an 11 lb (5 kg) payload capacity, the OmniRAM Pharma is a full-featured, digitally controlled batch mixer for larger-than-bench-scale development, clinical trials, pre-production, and small-scale production and processing. This makes it the ideal pharmaceutical workhorse for organizations running Phase I and Phase II clinical trials, where batch sizes have outgrown the PharmaRAM II but full RAM 5 Pharma production volumes aren't yet required. The OmniRAM Pharma ensures that the formulation quality, content uniformity, and process parameters established during early R&D are preserved and validated at clinical scale — so there are no surprises when the time comes to move to full production. Built on the Same World-Class Platform The OmniRAM Pharma is built on the same technology platform and operating system as Resodyn's PharmaRAM II, supporting repetitive and precursor processes and including vacuum and temperature monitoring capability. This shared platform is a critical advantage — it means operators who have worked on the PharmaRAM II need no additional training, and process parameters developed on the bench translate directly and predictably to the OmniRAM Pharma without re-testing or reformulation. RAM technology scales easily without additional testing from development to pilot to production scales. GMP Compliance & Data Integrity Built In The OmniRAM Pharma's onboard operating system provides pharmaceutical manufacturers with the full suite of data management and security tools required for GMP-compliant operations. Recipe development, storage, and security ensure that every batch is produced to exactly the same validated parameters — a requirement for clinical trial material manufacturing and eventual regulatory submission. Real-time parameter monitoring and 100% processing data retention give quality assurance teams complete batch traceability from start to finish. RAM ensures uniform distribution of active pharmaceutical ingredients even at low concentrations — such as below 1% — helping maintain dose accuracy and content uniformity, which are critical for tablet and capsule formulations. For clinical trial material where dosing precision can directly affect patient outcomes and trial data integrity, this level of uniformity is not optional — it is essential.
CATEGORY
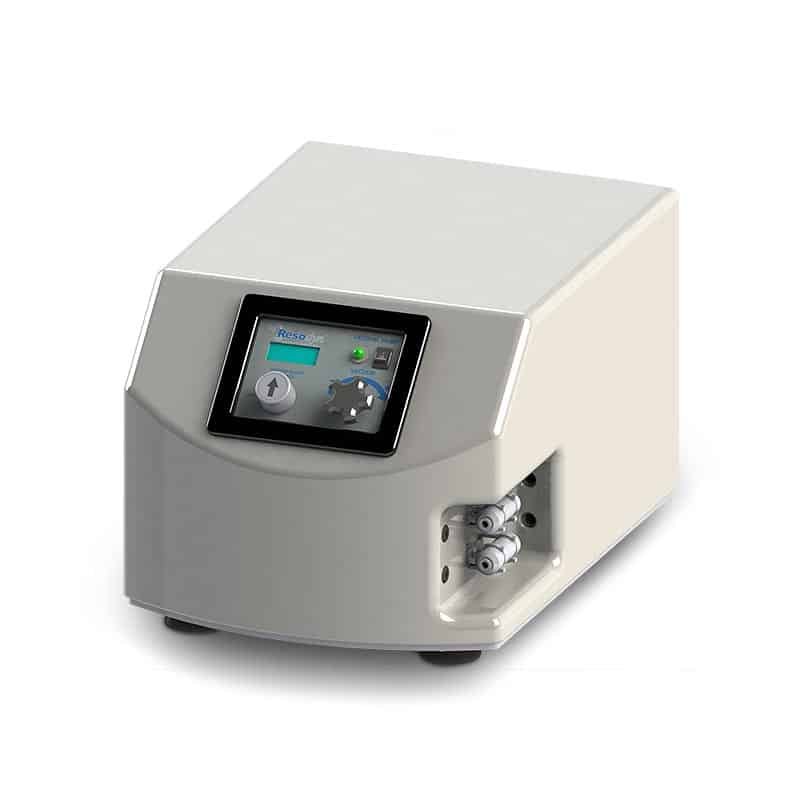
Automated, recipe-based vacuum control for virtually any materials processing.
CATEGORY
