By Touchstone Research Laboratory
Metric Nominal Density: ISO 12985-2, g/cc, 0.4 – 0.6 Compressive Strength: ISO 18515, MPa, 1.5 – 1.8 Compressive Modulus: ISO 18512, MPa, 100 – 400 Tensile Strength: ISO 12986-2, MPa, 0.9 – 1.0 Shear Strength: ISO 12986-2, MPa, 1.0 – 4.0 Coefficient of Thermal Expansion: ISO 14420, ppm/°C, 2 Thermal Conductivity: ASTM E 1461, W/m-K, 106 W/m-K at 0.47 g/cc Maximum Operational Use Temperature: Environment Dependent, °C, 400 Electrical Resistivity: ISO 11713, milliohm-cm, 3 – 4 Pore Volume: Microscopy, %, >70% Mean Pore Size: Microscopy, Microns, 1,200 US Nominal Density: ISO 12985-2, lbs/ft 3, 25 – 35 Compressive Strength: ISO 18515, psi, 218 – 261 Compressive Modulus: ISO 18512, ksi, 14 – 58 Tensile Strength: ISO 12986-2, psi, 130 – 145 Shear Strength: ISO 12986-2, psi, 145 – 580 Coefficient of Thermal Expansion: ISO 14420, ppm/°F, 1.1 Thermal Conductivity: ASTM E 1461, W/m-K, 106 W/m-K at 29 lbs/ft 3 Maximum Operational Use Temperature: Environment Dependent, °F, 750 Electrical Resistivity: ISO 11713, milliohm-in, 1.2 – 1.6 Pore Volume: Microscopy, %, >70% Mean Pore Size: Microscopy, Inches, 0.05
As a unique acoustic absorption material, CFOAM may be utilized in shipbuilding, aerospace, and automotive industries. A one-inch thick CFOAM panel will absorb between 20-60% of a soundwave directed at it. Increasing the thickness of the foam can yield absorption values closer to 100%, and its high density relative to most polymer foams makes it well-suited for absorbing sound at lower frequencies. Given its excellent fire resistance, low thermal conductivity, low density, and high strength, CFOAM offers a state-of-the-art material system for many applications requiring sound absorption.
CATEGORY
CFOAM’s high strength at low density and inherent crushability provides significant energy absorbing properties in composite structures where it can be used as a core. CFOAM’s blast and crash resistant properties and performance continues to be researched for application in ground vehicles, aircraft, ships, infrastructure, shelters, cargo areas, and trains.
CATEGORY
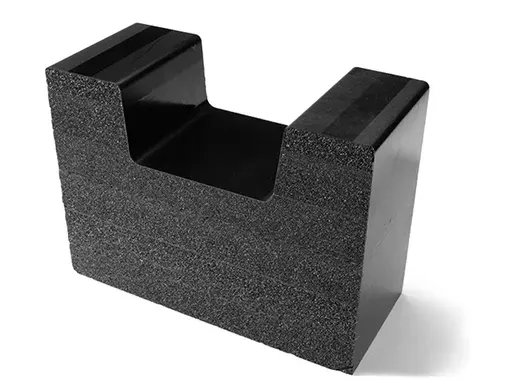
Faster tooling. Stable geometry. Lower total cost. CFOAM enables a different approach to composite tooling. Instead of machining heavy metal and managing thermal inertia, engineers can build dimensionally stable, lightweight tools that machine easily, and scale without penalty. For carbon fiber layup, mandrels, and cure tools, CFOAM removes many of the constraints that have historically driven up cost and lead time. Why Engineers Choose CFOAM Composite Tooling with Clear Benefits Low CTE Where It Matters CFOAM maintains a coefficient of thermal expansion (CTE) near 2.8 ppm/°F, allowing tools to track composite parts closely through cure cycles. This reduces residual stress, improves dimensional accuracy, and minimizes iterative rework. Machinability Without Penalty CFOAM machines easily. Large billets can be bonded, shaped, and quickly modified. Design changes that would be cost-prohibitive in metal become routine. Lightweight at Scale At roughly 30 lbs/ft3, CFOAM tools are dramatically lighter than metal equivalents. This simplifies handling, reduces fixture requirements, and enables larger tool geometries without infrastructure changes. Cost Advantage Without Compromise Prototype tools have been demonstrated to have significant cost and lead time savings than Invar, while maintaining performance in real composite manufacturing environments. The Key Technical Advantage A Different Tooling Physics Conventional Tooling Dimensional Stability Thermal Responsiveness Manufacturability Most tooling materials force a tradeoff between dimensional stability, thermal responsiveness, and manufacturability. CFOAM Tooling Low CTE Low Density Machinable Structure CFOAM combines low CTE (dimensional control), low density (low thermal inertia), and machinable structure (fast iteration) without tradeoffs. For tooling programs limited by lead time constraints, rework, or modification cost, CFOAM is not simply a material substitution. It can change the cost, schedule, and flexibility profile of the entire tooling workflow. How CFOAM Tooling Is Built Proven Tool Construction Workflow Billet Formation Blocks are bonded into near-net shapes, enabling large tools without material constraints. Rough CNC Machining Geometry is cut efficiently with standard tooling. Surface Build-Up Carbon prepreg or a carbon filled epoxy resin are applied to create either a durable production style tool face, or a rapid prototype production option. Autoclave Cure The surface layer is consolidated under production-like conditions. Final Machining and Finishing Precision geometry is achieved, followed by sealing and polishing for release-ready surfaces. This hybrid approach combines the structural benefits of CFOAM with the surface performance of composite tooling systems. The prototype version is perfect for developmental programs as this tooling method is easily modifiable to support evolving engineering. It can then be "recycled" to convert it to production tooling by using the same base CFOAM material, then wrapping it with carbon prepreg adding durability with cost and lead time savings by repurposing the prototype version. Performance in Practice Validated in Composite Tooling Applications CFOAM has been used in hundreds of tooling builds, including complex geometries that would be difficult or costly in metal. - Large, multiple piece breakdown mandrels - Stable performance through repeated cure cycles - Reliable part release with standard surface treatments - Comparable surface hardness to traditional composite tooling systems CFOAM vs Traditional Tooling Materials Where CFOAM Wins: Performance Benefits CFOAM vs. Invar CFOAM vs. Aluminum CFOAM vs. Composite Tools (all-prepreg) CFOAM vs. Invar - Lower cost - Faster machining - Faster thermal response - Much lower weight - Faster lead times CFOAM vs. Aluminum - Lower CTE - Better dimensional stability across cure cycles CFOAM vs. Composite Tools (all-prepreg) - More stable core structure - Easier large-scale machining - Better repeatability in thick sections Design Flexibility Engineered, Not Just Selected CFOAM is not a single fixed material. Density, pore structure, and surface treatments can be tailored for each application. This allows engineers to optimize stiffness vs weight, permeability and vacuum integrity, surface integration strategies, and thermal response characteristics. The Key Perspective Tool performance is not just about the base foam. The surface system and integration method determine final performance. CFOAM enables more control over that system than traditional tooling materials. Practical Considerations A number of well-understood processes are already built into standard CFOAM tooling workflows. Such as surface sealing is required for vacuum and finish quality, and bonding and surfacing processes should be controlled for durability. Where CFOAM Fits Best CFOAM delivers the most value when: - Tools are large or complex - Iteration speed matters - Weight or handling is a constraint CFOAM is especially effective for: - Carbon fiber layup molds - Mandrels - Autoclave tooling - Prototype-to-production transitions Is CFOAM Composite Tooling Right For You? CFOAM is not just a substitute for metal tooling. It enables a different design and manufacturing approach. If your current tooling strategy is limited by cost, weight, or thermal performance, it's time to rethink these tooling constraints. CFOAM is worth evaluating early in the design process.
CATEGORY
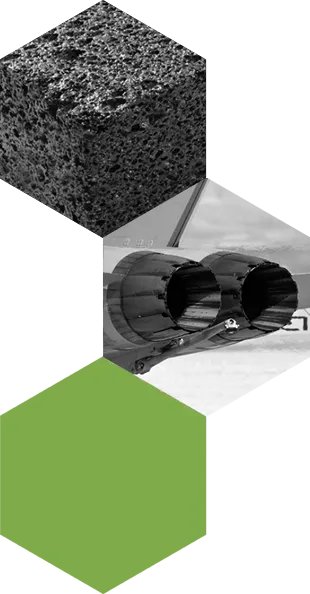
CFOAM® HTC graphite foam – a graphitized, lightweight, open-cell carbon foam produced from mesophase pitch that features an exceptionally high thermal conductivity of about 100 W/m-K at room temperature with significant weight savings in comparison to copper (22 times lighter) and aluminum (7 times lighter). CFOAM HTC also has relatively high electrical conductivity, good strength, and a low coefficient of thermal expansion. It is easily machinable, chemically inert, corrosion free, and resistant to harsh environments and oxidation up to 400°C. With the infusion of a phase change material into its porosity, heat capacity can be greatly increased without a significant weight penalty. Manufactured at a scale, cost, and commercial output rate designed to penetrate already identified markets, CFOAM HTC graphite foam supports: - Thermal management heat sinks for application such as LED lighting, reducing weight and increasing life. - Lightweight and efficient heat exchangers for military applications. - Industrial heat exchangers for enhanced thermal heat transfer in single or multi-phase industrial heat exchanger products. - Electronics component cooling. - Automotive applications providing enhanced cooling in a smaller, lighter weight unit. - Solar, improving photovoltaic panel efficiency.
CATEGORY
